Piezoresistive Pressure Sensor Humidity Drift Mitigation Fundamentals
Piezoresistive humidity drift stems from polymer swell stresses across the die; mitigate it with inorganic barrier films, compliant bonds, or oil isolation.
Swell
Piezoresistive pressure dies bonded to ceramic or leadframe substrates shift their zero-point balance when ambient moisture penetrates packaging polymers. Water absorption creates volume expansion in die-attach adhesives, silicone encapsulation gels, and overmolding compounds. This swelling generates mechanical strain that couples directly into the micro-machined silicon diaphragm.
Silicon exhibits piezoresistive coefficients where mechanical stresses alter carrier mobility in diffused p-type or n-type resistors. An asymmetrical transverse stress of 1 MPa across a p-type Wheatstone bridge induces an electrical offset shift exceeding 0.05% of full scale span. Moisture diffusion proceeds gradually, driven by relative humidity gradients and elevated ambient temperatures, converting ambient humidity cycles into erratic zero-point wander.
Die-attach adhesives represent the most immediate path for asymmetric strain transfer. Epoxies absorb between 0.5% and 3.0% moisture by weight at saturation in 85% relative humidity environments. As water molecules hydrate polymer chains, the adhesive matrix expands according to its coefficient of hygroscopic swelling.
Glass transition temperatures drop simultaneously via plasticization, softening the bondline while shifting its shear modulus from 3.5 GPa down to 1.8 GPa. Because silicon maintains a hygroscopic expansion coefficient of zero, the differential swelling between the swelling epoxy and the rigid silicon base induces bimetallic-type bending moments directly across the diaphragm membrane.
Silicone gel absorption coefficients dictate the recovery baseline of piezoresistive bridges.
Encapsulation materials present secondary mechanical coupling paths. Piezoresistive dies designed for harsh media protection frequently employ soft silicone gels to shield aluminum bond pads and wire bonds from liquid condensation and ionic contaminants. Silicone gels exhibit low elastic moduli below 100 kPa.
Their bulk thermal and hygroscopic volume changes transmit hydrostatic pressure components directly to sensitive silicon diaphragms when gel wells are constrained by rigid metal or premolded plastic sidewalls. Unconstrained gel surfaces swell upward, while lateral constraints redirect volumetric expansion toward the diaphragm surface, driving false positive gauge pressure readings during relative humidity upswings.
Hygroscopic Stress Coupling Mechanisms
The total strain field acting upon diffused piezoresistors combines intrinsic packaging stress, thermal mismatch stress, and hygroscopic expansion strain. Modeling the hygroscopic component follows Fickian diffusion equations:
∂C/∂t = D · ∇²C
The local concentration C of moisture governs the free hygroscopic strain ε_h through the coefficient of chemical expansion β, defined as:
ε_h = β · C
When moisture concentration exhibits a spatial gradient across the die mount, the induced bending moment M_h introduces differential surface stresses across the four active piezoresistors of the Wheatstone bridge. Silicon membranes etched to thicknesses between 5 µm and 30 µm respond to minute out-of-plane moments. If moisture ingress occurs symmetrically from all perimeters, stresses cancel at the geometric center of balanced four-resistor layouts.
Die placement tolerances, adhesive fillet asymmetries, and voiding within the bondline break this symmetry. Die bond voiding of 5% creates localized compliance paths, transforming uniform environmental moisture absorption into pronounced differential stress fields across opposing bridge arms.
Silicone potting formulations carry varying moisture absorption capacities. Phenyl-based silicones display lower moisture diffusion rates than dimethyl-based alternatives while exhibiting higher bulk moduli. Dimethyl silicones transmit minimal shear stress due to extreme compliance, yet water accumulates rapidly along the silicon-gel interface.
Moisture pooling at this interface compromises native silicon oxide passivations and initiates surface charge redistribution, producing electrical zero wander through surface parasitic leakage alongside mechanical strain.
- Hygroscopic bondline expansion drives localized mechanical distortion into the die edge, generating uncalibrated offset drift across operating moisture cycles.
- Adhesive plasticization effects alter the mechanical coupling factor between die and substrate, permanently modifying factory-trimmed temperature coefficients of span.
- Interfacial delamination mechanics initiate micro-gaps beneath the silicon pedestal, generating severe non-repeatability during subsequent dry-out phases.
- Constrained gel volume growth converts relative humidity spikes into false positive line pressure signals through hydrostatically confined packaging cavities.
Curing conditions determine the baseline dry state of packaging polymers. Elevated cure temperatures lock high thermal stresses into die bonds upon cooling to ambient levels. Subsequent ambient moisture exposure reduces the effective tensile stress in the adhesive via hygroscopic swelling, acting as an apparent stress relief mechanism.
Dry conditions reverse this relief, contracting the polymer and restoring elevated bondline stress states. The bridge experiences continuous stress cycles without pressure changes.
Thick adhesive layers multiply overall hygroscopic displacement.
Passivation
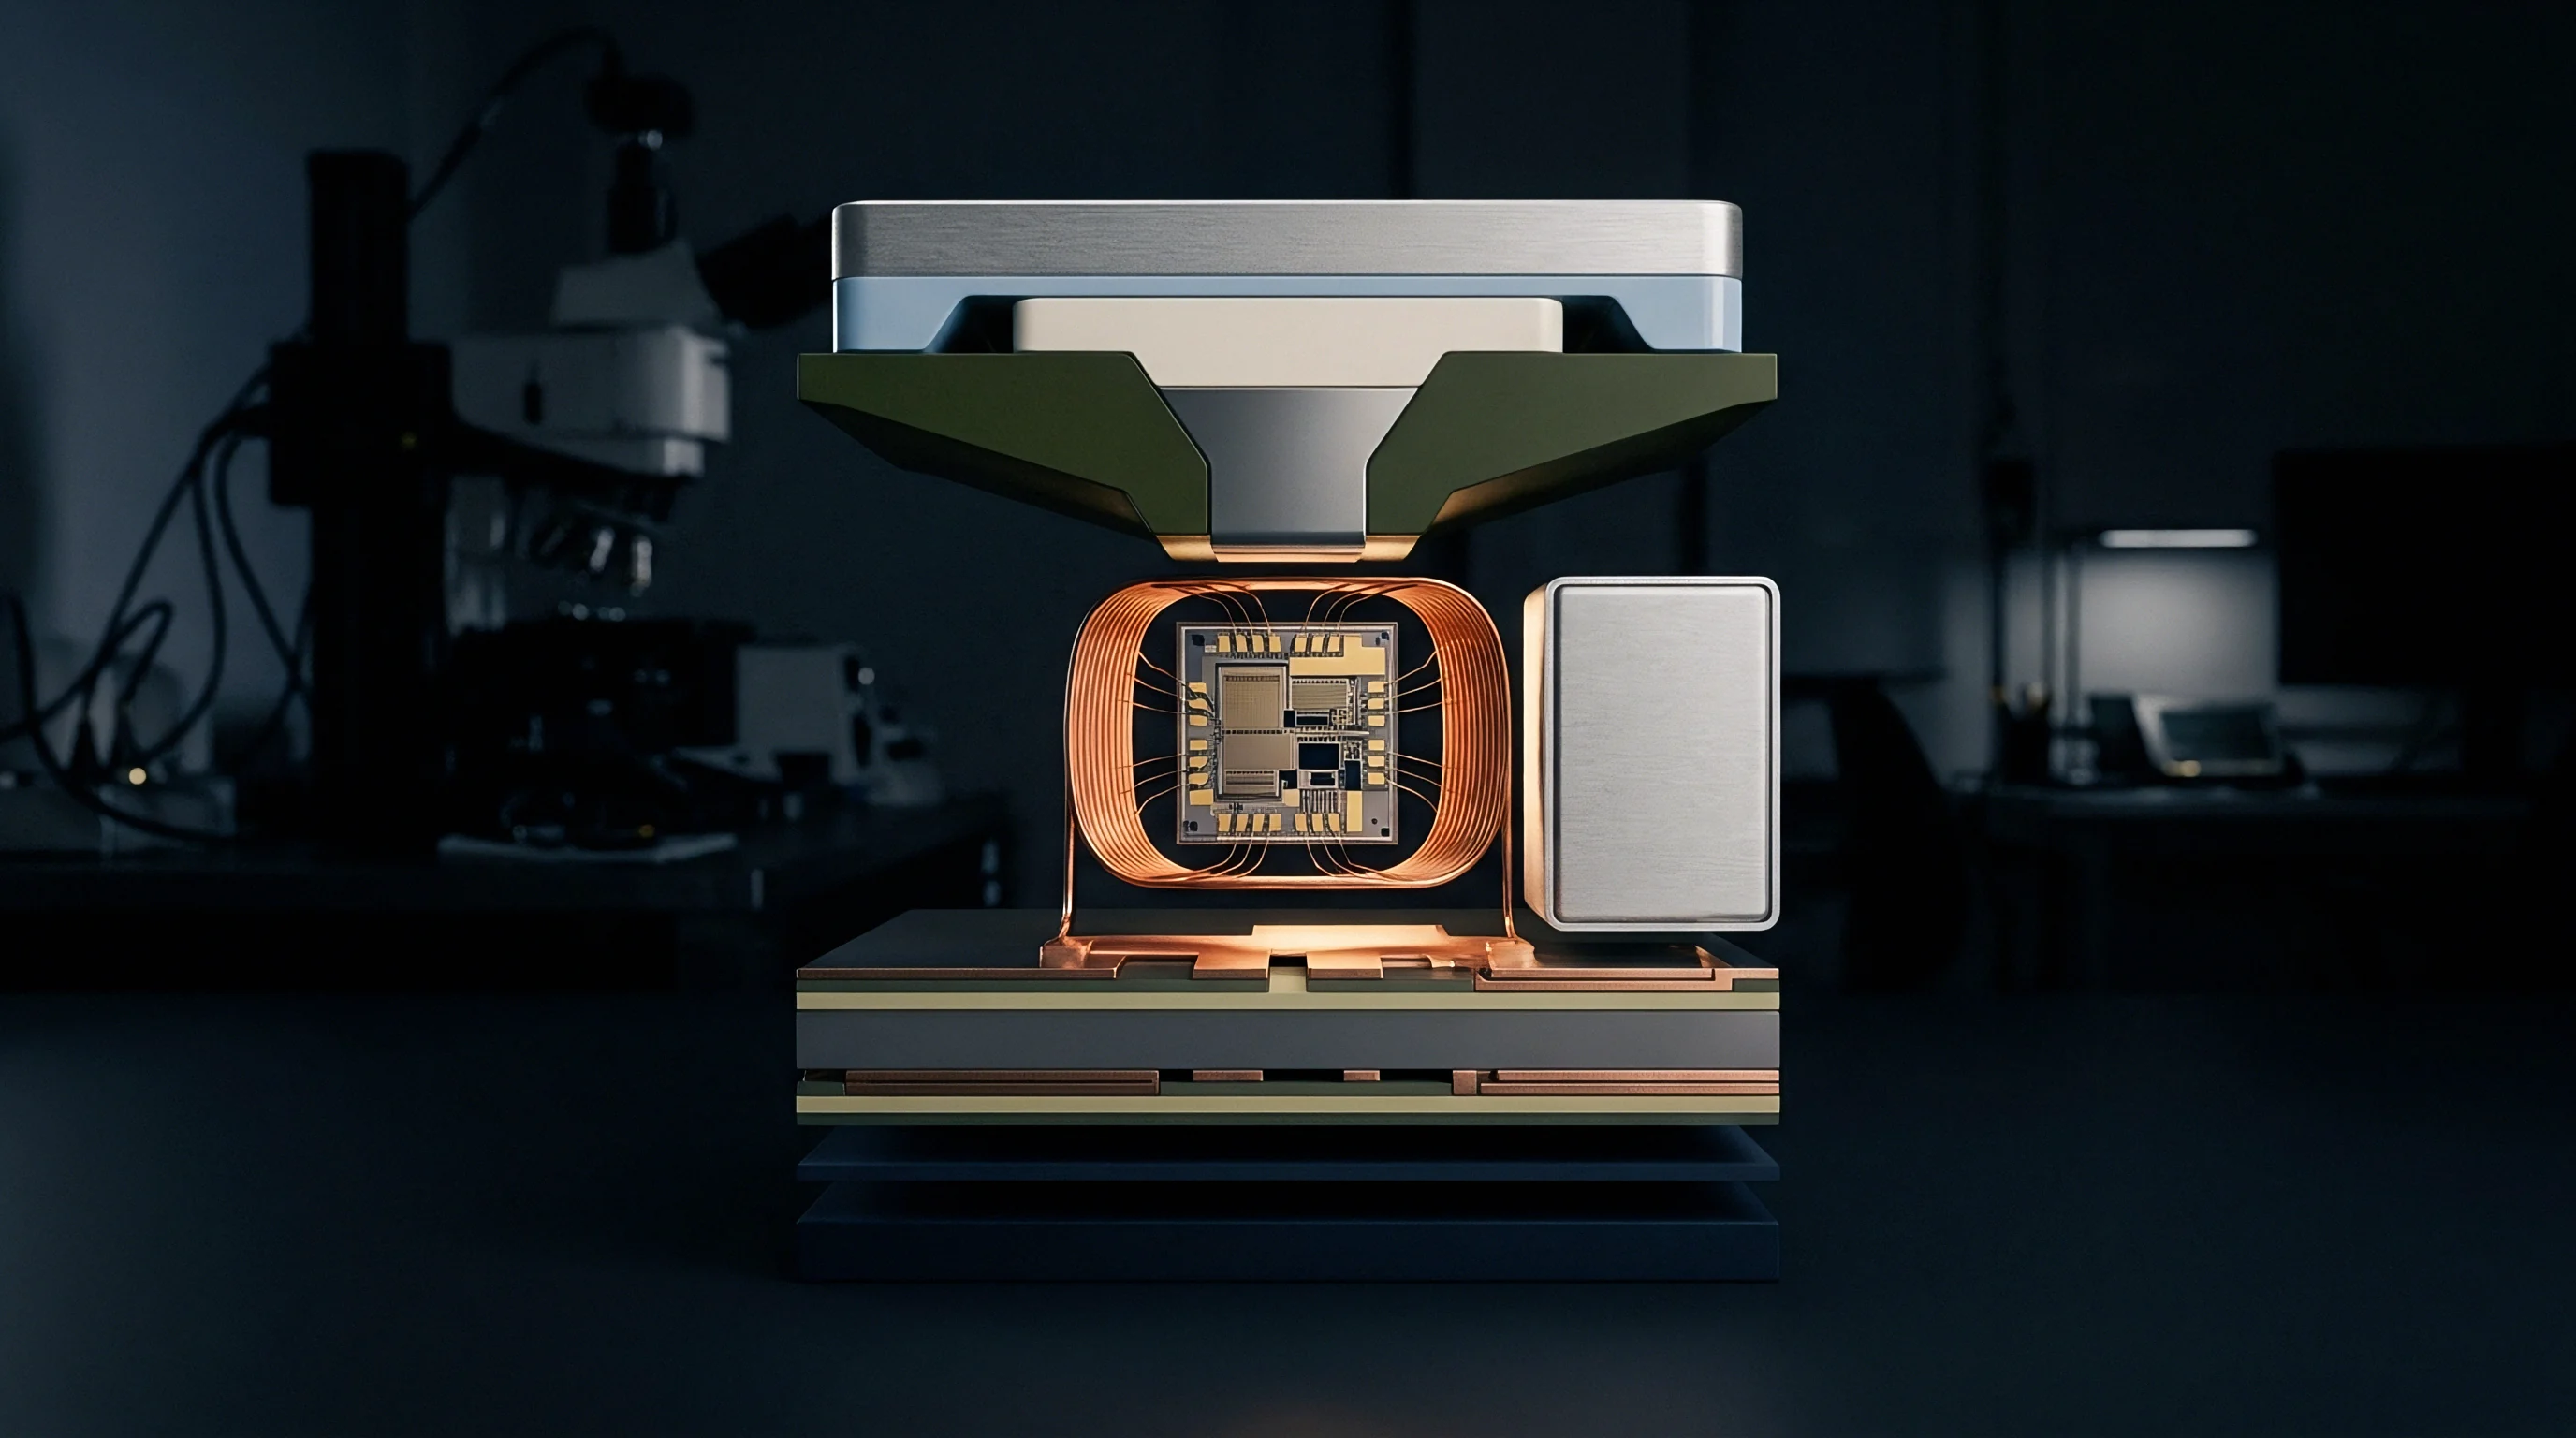
Barrier coatings isolate piezoresistive elements from moisture ingress. Standard silicon dioxide layers grown thermally on silicon offer effective electrical insulation against dry air, but ambient water vapor hydrolyzes siloxane bonds to form silanol groups under sustained high-humidity conditions. Silicon nitride deposited via low-pressure chemical vapor deposition exhibits high atomic density, providing an effective inorganic barrier against water permeation.
Stoichiometric silicon nitride films of 150 nm thickness suppress moisture penetration to negligible levels across standard sensor operational lifespans. Residual film stress within silicon nitride layers must balance against the diaphragm mechanical profile to avoid introducing high offset drift or diaphragm buckling.
Parylene deposition provides conformal organic barrier protection across fully wire-bonded die assemblies. Vapor deposition polymerization applies poly-para-xylylene uniformly over three-dimensional geometries without pinholes, meniscus formations, or edge thinning. Parylene C displays a water vapor transmission rate of 0.08 g·mm/(m²·day) at 37°C and 90% relative humidity, outperforming epoxies and polyimides by two orders of magnitude.
The film coats bond wires, package sidewalls, and silicon diaphragm surfaces in a single vacuum process.
Parylene C films applied above three micrometers thickness shift diaphragm resonance and alter calibrated pressure sensitivity.
Film thickness demands precise control during deposition runs. Thin layers below 1 µm leave step coverage defects over sharp silicon edges and wire bond heels. Heavy layers above 5 µm add mechanical stiffness to thin silicon diaphragms, reducing pressure sensitivity and introducing secondary thermal hysteresis errors driven by the high thermal expansion coefficient of Parylene.
Industrial implementations target uniform coatings between 2 µm and 3 µm to achieve moisture isolation while preserving factory calibration accuracy.
Has Silicone Gel Reached Inherent Saturation Limits?
Silicone potting gels cannot prevent moisture entry. Water vapor diffuses through polysiloxane networks rapidly, reaching equilibrium saturation within hours of environmental exposure. Silicones function by providing low surface energy passivations that prevent liquid water condensation and stop mobile ionic contaminants from forming conductive aqueous pathways across bare metallizations.
Water vapor passes through the molecular interstices of the gel and arrives at the silicon interface as gaseous molecules.
| Material Class | Water Vapor Transmission Rate (g·mm/m²·day) | Young Modulus (MPa) | Moisture Absorption at Saturation (%) | Adhesion Stability Under Moisture |
|---|---|---|---|---|
| Thermal Silicon Nitride | 0.00001 | 290000 | 0.01 | Permanent chemical bond |
| Parylene C | 0.08 | 3200 | 0.06 | Silane primer dependent |
| Die-Attach Epoxy (High Modulus) | 1.80 | 4500 | 1.60 | Degrades via plasticization |
| Die-Attach Silicone (Low Modulus) | 15.00 | 2.5 | 0.30 | Moderate interface retention |
| Dimethyl Encapsulation Gel | 45.00 | 0.05 | 0.15 | Cohesive interface cavitation |
Advanced media-isolated designs eliminate direct polymer exposure by utilizing metal diaphragms and oil fill fluids. A thin corrugated diaphragm fabricated from 316L stainless steel, Hastelloy C-276, or titanium isolates the process environment entirely. A vacuum-degassed silicone or synthetic hydrocarbon oil transmits external hydraulic pressure to a dry-cavity silicon die positioned within a hermetically sealed header.
Moisture cannot permeate welded metal diaphragms or glass-to-metal electrical feedthroughs. The oil-filled architecture eliminates packaging-induced hygroscopic strain at the expense of higher component costs, increased physical footprint, and larger thermal expansion errors caused by oil volume changes.
Packagers frequently explain that ambient water molecules will pass through any gel layer within two days of warehouse storage.
Chamber
Verification of humidity drift performance demands environmental exposure protocols. Manufacturers typically execute high-temperature operating life tests alongside steady-state damp heat qualifications. The baseline international procedure IEC 60068-2-78 establishes continuous exposure criteria, requiring unpowered or powered sensor dwell at 40°C and 93% relative humidity for durations of 240, 504, or 1000 hours.
The test isolates steady-state water permeation kinetics, revealing the ultimate zero-point offset shift once packaging polymers reach moisture saturation.
Automotive and industrial qualification procedures frequently employ IEC 60068-2-30 cyclic damp heat testing. This standard subjects components to 24-hour temperature cycles between 25°C and 55°C (or 65°C) at relative humidity levels maintained above 90%. Temperature swings force moisture ingress during cooling phases through condensation and localized pressure differentials within unsealed package cavities.
Cyclic testing exposes breathing effects within semi-hermetic sensor enclosures, accelerating delamination along die-attach perimeters and driving severe mechanical hysteresis.
- Pre-exposure baseline calibration records bridge offset, full scale span, and temperature coefficients across the full compensated temperature window inside dry gas.
- Controlled ramp and dwell execution subjects devices to specified damp heat levels within an environmental chamber while logging real-time bridge output signals at constant applied atmospheric pressure.
- Intermediate electrical verification assesses zero wander at defined inspection intervals without removing devices from conditioned chamber atmospheres.
- Post-dwell stabilization sequence brings devices back to ambient room conditions (23°C and 50% relative humidity) under continuous monitoring to observe desorption recovery trajectories.
- Final calibration extraction recalculates residual zero-point errors, span shifts, and non-linearity deviations against baseline values to determine unrecoverable degradation.
Hysteresis Quantification and Recovery Profiles
Hygroscopic drift exhibits pronounced temporal hysteresis. Moisture absorption proceeds along rate constants determined by polymer diffusion coefficients and geometric path lengths. Desorption curves rarely mirror absorption timelines.
Water molecules form hydrogen bonds with polar groups within epoxy and polyimide matrices, slowing desorption during dry-out phases.
IEC 60068-2-78 exposure at 40°C and 93% relative humidity for 1000 hours reveals irreversible chemical shifts in unpassivated die bonds.
Plastic deformation within the adhesive matrix during saturated swelling prevents the bridge from returning to its original zero point even after total moisture removal. An unpassivated piezoresistive sensor exposed to an 85°C and 85% relative humidity dwell for 500 hours may experience an offset shift of 0.45% of span at saturation. Following a 48-hour bake-out at 60°C in dry nitrogen, the sensor often retains an irreversible residual offset of 0.12% of span.
The unrecoverable shift represents permanent micro-structural alterations within the polymer network and localized adhesive bondline yield.
Test protocols must distinguish between reversible hygroscopic offset drift and unrecoverable packaging degradation. Measuring recovery kinetics across extended stabilization periods provides direct visibility into bondline integrity. Devices displaying rapid zero-point recovery maintain intact interfaces, whereas devices exhibiting prolonged recovery tails or stepped offset shifts demonstrate interfacial delamination along the die-attach fillet.
Can automated chamber cycling accurately predict three-year outdoor drift when seasonal humidity shifts combine with daily thermal swings?
Offset
Modern pressure transmitters employ digital signal conditioning application-specific integrated circuits (ASICs) positioned adjacent to the piezoresistive sensing bridge. These ASICs incorporate high-resolution analog-to-digital converters, programmable current or voltage excitation sources, and internal non-volatile memory storing calibration coefficients. Factory calibration sequences typically populate multi-order polynomial compensation matrices that correct for bridge offset, span non-linearity, and thermal shifts across the operating temperature window.
Standard compensation architectures fail to resolve moisture-induced errors because conventional pressure ASICs lack humidity inputs. A piezoresistive bridge subjected to 85% relative humidity shifts its zero balance through mechanical strain. The ASIC measures this resistance shift as an applied pressure change or a thermal deviation.
The conditioning circuit corrects thermal shifts through on-chip temperature sensors. If the ambient temperature remains constant while moisture levels climb, the circuit transmits the hygroscopic strain directly to the output register as raw line pressure.
Integrated Environmental Compensation Structures
Mitigating uncompensated humidity drift at the silicon level requires localized relative humidity monitoring. Advanced transmitter designs integrate a capacitive relative humidity sensor directly onto the pressure ASIC or alongside the piezoresistive bridge within the same package enclosure. The integrated humidity cell provides real-time local moisture concentration data to the digital core, allowing two-dimensional polynomial compensation:
V_out = Σ Σ A_ij · P^i · T^j + Σ B_k · RH^k
The coefficients B_k capture the empirical offset response of the specific package configuration under moisture variations. This firmware correction reduces steady-state humidity drift by 70% to 85% across moderate operational bands.
| Mitigation Architecture | Typical Offset Drift (1000h 85/85) | Initial Unit Cost Adder | Assembly Complexity | Calibration Time Adder |
|---|---|---|---|---|
| Standard Silicon Die, Bare Epoxy | 0.60% to 1.20% Span | Reference Baseline | Standard SMD Line | Zero (Standard Cal) |
| Parylene C Vapor Coating (3 µm) | 0.08% to 0.15% Span | 1.25x Baseline | Vacuum Batch Step | Zero (Standard Cal) |
| ASIC Humidity Sensor Integration | 0.10% to 0.20% Span | 1.40x Baseline | Dual-Die Package | 2.5x (Chamber RH Steps) |
| Welded Oil-Filled Metal Header | 0.01% to 0.03% Span | 3.10x Baseline | Specialized Header Line | 1.8x (Oil Expansion Trim) |
Firmware-based compensation carries distinct processing limitations. Dynamic moisture absorption lag complicates compensation algorithms. Ambient humidity changes register immediately on surface capacitive sensors, while moisture diffusion into thick die-attach bondlines exhibits time constants ranging from hours to weeks.
Applying real-time offset corrections based on instantaneous capacitive readings introduces transient errors during rapid humidity transitions.
Algorithmic zero-tracking routines offer alternative software mitigation in cyclic applications. In barometric, HVAC, and cleanroom monitoring scenarios, line pressure periodically returns to atmospheric baselines or known differential zeros. Firmware routines track the slow drift of this reference point over rolling 30-day windows.
The algorithm filters out high-frequency pressure changes while adjusting zero-trim registers to counteract gradual hygroscopic drift. The baseline tracking method functions continuously without dedicated relative humidity sensors.
Algorithmic zero-tracking operates successfully only when processes provide frequent, verifiable zero-pressure conditions during scheduled operation.
Warranty
Uncontrolled zero drift generates heavy commercial exposures for instrumentation procurement programs. Precision pressure transmitters specified at 0.1% full scale accuracy operate in outdoor, marine, and process environments where relative humidity ranges between 10% and 98%. If an unmitigated sensor package drifts 0.5% of span over twelve months of field deployment, the device exceeds its published accuracy class by a factor of five.
End users reject batches, dispute quality records, and trigger warranty replacement clauses.
Field recalibration costs dwarf initial component procurement savings. Deploying instrumentation technicians to recalibrate drifting pressure transmitters across remote pipeline stations or cleanroom facilities costs hundreds of dollars per measurement point. When sensors drift beyond re-zeroing thresholds, entire sensor subassemblies require field extraction, shop recalibration, or outright replacement.
A procurement team saving two dollars per sensor by accepting bare epoxy die-attach packaging transfers ten times that margin to service budgets within two years.

Procurement Verification and Acceptance Specifications
Procurement contracts must bind suppliers to verifiable stability thresholds under defined damp heat environments. Standard vendor datasheets quote initial accuracy at 25°C in dry laboratory air, masking moisture susceptibility behind generic long-term stability claims. A comprehensive specification isolates environmental drift through precise testing criteria.
- Saturation offset stability defines maximum allowable bridge offset shift after 504 hours of exposure to 85°C and 85% relative humidity, bounding uncompensated zero error.
- Desorption recovery limits enforce minimum return tolerances toward baseline zero following a 24-hour dry-out period at standard laboratory conditions.
- Compensated span boundaries restrict thermal sensitivity degradation caused by moisture-induced adhesive plasticization and bondline modulus shifts.
- Ingress barrier verification mandates helium leak or fluorocarbon bubble testing for hermetic packages, and dielectric breakdown confirmation for conformal coatings.
Rigorous qualification demands formal compliance validation. Factory acceptance testing protocols require random sample screening from incoming lots. Test samples undergo accelerated damp heat dwells within calibrated climatic chambers, with outputs verified against traceable pressure references before and after environmental dwells.
Lots exhibiting offset shifts beyond agreed tolerance guardbands face immediate commercial rejection at the incoming inspection dock.
Purchasers protect capital budgets by inserting explicit damp-heat drift limits into supply contracts, requiring that long-term stability specifications remain fully valid across relative humidity bands up to 95% non-condensing throughout the entire warranty duration.