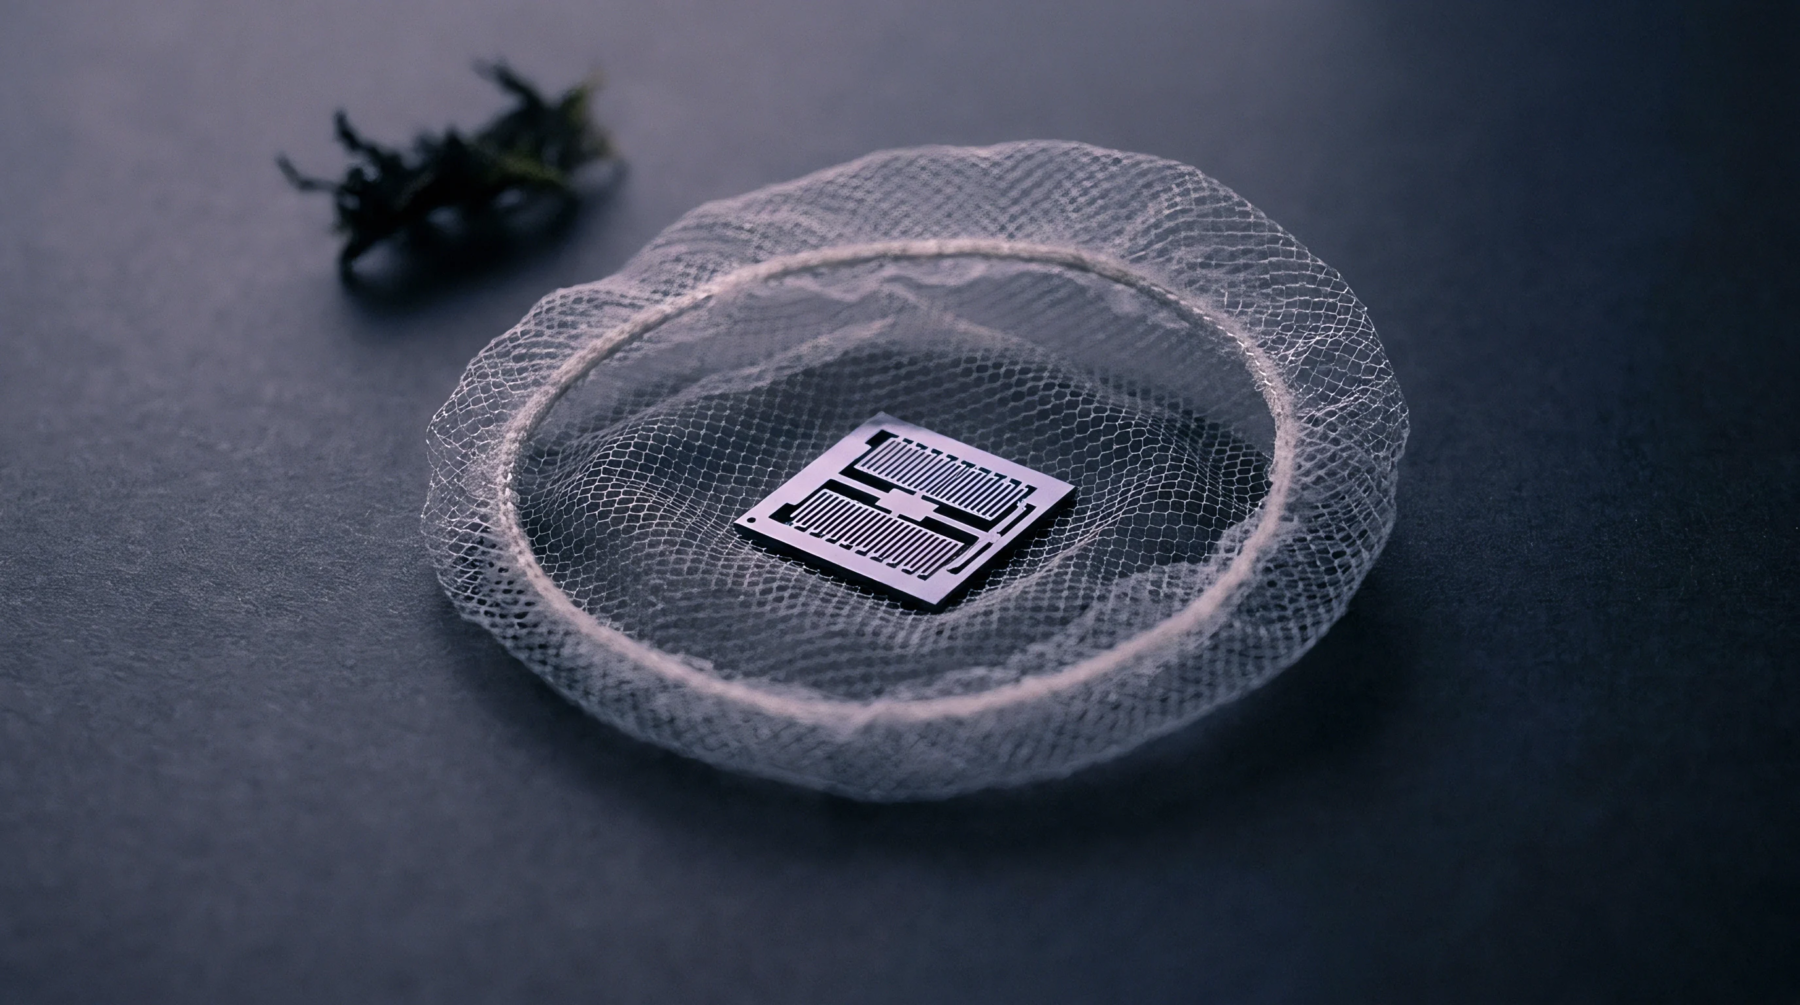
Metrological Extent
Operational boundaries define the active die area through precise lithographic limits established by semiconductor manufacturing equipment during wafer patterning. Measurement systems evaluate this functional region by detecting photocurrent generation and electrical continuity across integrated circuitry. Optical metrology tools verify dimensional compliance against photomask design intent under standardized laboratory lighting.
Thermal expansion during operational testing induces mechanical stress that shifts the outer boundary of this functional zone away from nominal coordinates. Edge distortion from chemical etching introduces permanent measurement errors that calibration routines must isolate from actual silicon dimensions. Semiconductor fabrication facilities establish strict boundary tolerances using laser interferometry to maintain submicron verification accuracy.
Current Distribution
Charge carrier movement across the active die area generates localized thermal gradients that degrade signal fidelity in adjacent circuit blocks. High current densities concentrate near gate oxide interfaces during heavy switching cycles, accelerating localized electromigration phenomena. Voltage drops accumulate along long metallic interconnects because sheet resistance introduces predictable potential losses across the silicon surface.
Automated test equipment measures leakage currents to verify that dielectric breakdown has not breached internal isolation barriers. Signal propagation delays correlate directly with thermal dissipation efficiency across the functional region during high frequency operation.
Yield Verification
Defect density calculations scale inversely with the total available active die area on processed silicon wafers. Optical inspection systems flag particulate contamination that bridges microscopic conductive traces within the functional boundary. Functional testing protocols apply worst case voltage margins to expose latent manufacturing flaws before packaging operations begin.
Electrical screening sequences isolate marginal components by comparing operational parameters against strict statistical process control limits. Automated sorting machinery discards defective silicon units based on pass or fail criteria recorded at multi pin probe stations.
Packaging Interface
Wire bonding equipment aligns interconnect terminals to contact pads positioned along the periphery of the active die area. Substrate thermal conductivity dictates how effectively heat dissipates away from the functional silicon into the surrounding package housing. Mechanical clamping forces exerted during encapsulation create compressive stresses that alter semiconductor bandgaps within the functional region.
Epoxy adhesion failures permit moisture ingress that corrodes internal metallic structures over extended deployment periods. Final metrology audits confirm that package assembly procedures preserve the electrical integrity established during initial wafer fabrication.