Polymer Encapsulation Mechanical Stress Mitigation in Industrial Sensing Assemblies
Compliant silicone buffer layers isolate piezoresistive silicon dies from rigid epoxy cure shrinkage, eliminating offset drift in harsh industrial sensors.
Resin
Polymer encapsulation protects sensitive industrial transducers from chemical ingress, vibration, and particulate contamination. The physical curing process of these potting formulations simultaneously introduces parasitic mechanical loads onto the underlying silicon elements. When an epoxy or polyurethane cross-links, polymer chains draw closer together, generating volumetric shrinkage between 0.5 percent and 4.5 percent depending on filler loading and resin chemistry.
This contraction creates compressive and shear stresses that transfer directly through the package header or substrate to the active sensing diaphragm or piezoresistive bridge. Raw transducer offset voltage drifts unpredictably when subjected to these uneven mechanical fields, degrading factory calibration before the device reaches field commissioning.
Rigid potting formulations with high Young’s modulus transfer ambient thermal expansion mismatches directly into the sensor die. High-performance industrial pressure and strain sensors rely on silicon piezoresistive elements having gauge factors exceeding 100, where a mechanical strain of 10 microstrain induces measurable output changes. Selecting an encapsulation material with an inappropriate glass transition temperature shifts the assembly into a glassy, high-modulus state within the operating temperature window.
Thermal cycling across this transition alters the baseline mechanical load, producing non-recoverable zero-point offset hysteresis that firmware algorithms fail to isolate from true physical measurands.
Peak hydrostatic pressure on the sensing diaphragm reaches 14.2 MPa when an unfilled cycloaliphatic epoxy cures inside an unvented aluminum housing at 120 degrees Celsius.
Viscoelastic Modulus and Glass Transition Selection
Encapsulation materials behave viscoelastically, displaying time-dependent and temperature-dependent modulus variations. Below the glass transition temperature, polymers exhibit an elastic modulus ranging from 1.0 GPa to over 10 GPa, behaving as rigid solids that transmit external housing deflections to internal wire bonds and die surfaces. Above the glass transition point, the polymer shifts to a rubbery state where the modulus drops by two to three orders of magnitude, typically falling between 1.0 MPa and 50 MPa.
Industrial sensing assemblies rated for operation between -40 degrees Celsius and 125 degrees Celsius require materials whose glass transition sits cleanly outside this span. Polymers with transitions inside the operating band induce sharp slope changes in the sensor temperature coefficient of offset.
Modulus selection balances mechanical isolation against environmental protection. Soft silicone gels present Young’s moduli below 0.5 MPa, dampening thermal shear stresses and preventing wire bond fatigue during extreme temperature swings. Silicone gels lack structural integrity, leaving the transducer vulnerable to high-pressure washdown jets, hydraulic fluids, and abrasive media.
Rigid epoxy systems provide chemical resistance and mechanical retention for terminal pins, but their high modulus concentrates stress at die corners. Formulators incorporate fused silica micro-fillers at 50 percent to 70 percent weight fractions, lowering the linear coefficient of thermal expansion from 65 ppm/K down to 18 ppm/K to closely match copper and ceramic carriers.
Piezoresistive Die Sensitivity under Hydrostatic Enclosure Load
Silicon dies exhibit anisotropic piezoresistive coefficients along standard crystallographic axes. Longitudinal and transverse stress components generated by curing polymers alter the resistivity of doped p-type channels in Wheatstone bridge configurations. Unequal resin distribution across the die surface creates asymmetric shear components, inducing substantial zero-load output shifts.
A standard 3.0 mm by 3.0 mm silicon pressure sensing die subjected to 5.0 MPa of asymmetric package stress experiences bridge imbalance exceeding 12 mV on a 5.0 V excitation rail, consuming over 20 percent of the analog-to-digital converter dynamic range before process calibration begins.
Hydrostatic pressure generated during high-temperature injection molding or transfer encapsulation introduces temporary compressive loading that relaxes slowly post-cure. As the polymer ages, secondary cross-linking and moisture absorption alter the hydrostatic baseline. Differential scanning calorimetry and thermomechanical analysis confirm that unoptimized cure schedules leave up to 8 percent unreacted monomer fractions.
Subsequent post-curing in field service shifts the zero-point voltage baseline by several millivolts over the first 500 operating hours.
Which Potting Chemistries Generate the Highest Solder Joint Shear?
Polyurethane and rigid epoxy chemistries generate the highest interfacial shear forces at the surface-mount component boundary. Polyurethanes cure with lower exotherms than epoxies, but their linear thermal expansion coefficients often exceed 100 ppm/K below their glass transition points. When thermal cycles swing from 20 degrees Celsius to -40 degrees Celsius, polyurethane potting contracts rapidly, imposing severe lateral displacement on discrete passive parts and small-outline integrated circuits.
Solder joint fatigue accelerates when thick polymer layers encapsulate leadless chip carriers and land grid array packages without stress-relief buffers. The thermal expansion delta between the FR4 circuit board (14 ppm/K in-plane), the alumina sensor die (6.5 ppm/K), and the polyurethane bulk (110 ppm/K) imposes cyclic plastic strain on SAC305 solder joints. Thermal shock qualification testing per JESD22-A106 reveals crack initiation along the component termination meniscus within 250 cycles when using unbuffered rigid potting.
Solder joint failure severs the analog frontend routing, permanently dropping transducer output signals.
| Polymer Chemistry | Young Modulus (MPa) | Linear CTE (ppm/K) | Glass Transition (C) | Volumetric Shrink (%) | Peak Exotherm (C) |
|---|---|---|---|---|---|
| Unfilled Bisphenol-A Epoxy | 3200 | 62 | 135 | 3.8 | 165 |
| Silica-Filled Epoxy (65 wt%) | 8500 | 22 | 155 | 0.8 | 110 |
| Two-Part Polyurethane | 450 | 105 | -25 | 1.5 | 65 |
| Dielectric Silicone Gel | 0.15 | 310 | -115 | 0.2 | 32 |
| Optically Clear Acrylate (UV) | 1800 | 85 | 72 | 4.2 | 45 |
Specifying a rigid epoxy without mechanical stress isolation cracks the sensor die corner fillets and destroys production yields during the initial thermal calibration run.
Shrinkage
Volumetric shrinkage originates at the molecular level during polymer polymerization and physical cooling. Monomer molecules held at van der Waals distances transition into covalently bonded polymer networks, reducing intermolecular spacing by 30 percent to 50 percent. Bulk volumetric contraction manifests across the curing profile as a combination of reaction shrinkage and thermal contraction.
Liquid epoxy resins dispensed at room temperature heat up rapidly due to exothermic cross-linking reactions. The polymer vitrifies at peak temperature, locking in a dense molecular structure that contracts severely as the assembly cools down to ambient factory floors.
Reaction kinetics determine the distribution of residual stresses throughout the sensing housing. Fast curing profiles driven by aggressive amine hardeners induce steep spatial temperature gradients across the potting depth. The exterior layer in contact with metal housing walls cools and vitrifies first, while the internal core continues its exothermic reaction.
This uneven cure sequence sets up severe tensile stresses at the potting core and compressive stresses along the assembly perimeter. The encapsulated sensing die experiences non-uniform triaxial loading that bends the silicon substrate.
Chemical Curing Kinetics and Volumetric Contraction
Monitoring resin shrinkage involves tracking the conversion rate of reactive epoxy or isocyanate groups. Fourier-transform infrared spectroscopy and rheometer profiles confirm that volumetric contraction scales linearly with monomer conversion until the gel point is reached. Before gelation, the liquid formulation flows to accommodate volume loss without accumulating internal mechanical stress.
Stress accumulation begins precisely at the gel transition, where the loss tangent drops and the polymer establishes a continuous three-dimensional cross-linked network.
Controlling the thermal ramp rate prevents premature vitrification. Curing an epoxy at a steady 60 degrees Celsius for four hours prior to a two-hour post-cure at 120 degrees Celsius allows molecular relaxation to dissipate shrinkage stresses during early network formation. Rapid single-stage curing at 130 degrees Celsius achieves full conversion in fifteen minutes, but freezes high internal stress fields directly into the housing cavity.
These internal stress fields distort internal bond wires, shifting their loop height and risking electrical short circuits against adjacent package leads.
Thermal Mismatch across Alumina PCB and Silicon Interfaces
Every industrial sensing assembly comprises multiple materials with widely divergent thermal expansion behaviors. Silicon exhibits a low linear expansion coefficient of 2.6 ppm/K, 96 percent alumina ceramic substrates expand at 6.5 ppm/K, and standard FR4 laminates expand at 14 ppm/K along the X and Y axes. Unfilled encapsulation resins exhibit expansion coefficients between 50 ppm/K and 120 ppm/K. Thermal changes inevitably induce intense shear stresses at every material boundary.
Biaxial stress at the die-attach interface is calculated via the Timoshenko bi-metal thermostat model. When the temperature falls 100 degrees Celsius below the zero-stress cure baseline, the polymer layer contracts significantly faster than the silicon die beneath it. The encapsulant pulls the edges of the die upward, inducing concave warping across the active sensing surface.
This mechanical warpage shifts piezoresistive resistor values on the die face by several hundred ohms, introducing large drift errors into high-precision 24-bit analog frontend measurements.
JEDEC JESD22-B106 solderability and mechanical integrity acceptance boundaries permit zero fillet cracking after ten consecutive solder dip cycles at 260 degrees Celsius.
Asymmetric Fill Geometries around Wire Bonds
Asymmetry in the potting cavity geometry creates unbalanced mechanical moments across sensitive internal connections. When an off-center dispense needle delivers resin to one side of a sensor cavity, the flow front pushes fine 25-micrometer gold or aluminum bond wires sideways. This wire sweep phenomenon causes adjacent wire loops to touch, resulting in intermittent analog input ground faults during final potted assembly vibration testing.
Uneven potting heights across the sensing die face generate bending moments that tilt the die relative to its mounting substrate. Bending moments alter the planarity of optical sensing arrays, magnetic Hall-effect elements, and capacitive pressure diaphragms. Standard industrial tolerances allow potting fill height variations of plus or minus 0.5 mm, a margin sufficient to induce measurable gain variations across multi-axis MEMS accelerometer sensors.
- Interfacial Delamination occurs when cure shrinkage shear stresses exceed the adhesive bond strength at the gold-plated pad interface, introducing air gaps that collect moisture.
- Silicon Die Cracking initiates at micro-cracks along diced die edges under concentrated tensile loads exerted by high-modulus unfilled epoxies during thermal shock.
- Bond Wire Necking manifests near the heel of wedge bonds as cyclic thermal expansion of the encapsulant pulls the wire vertically away from the substrate.
- Resistor Value Drift develops on thin-film passive networks when compressive polymer shrinkage alters sheet resistance through the piezoresistive effect.
Resin compounders consistently claim that cure shrinkage issues originate entirely from uncontrolled customer dispense temperatures and improper oven airflow rates.
Buffer
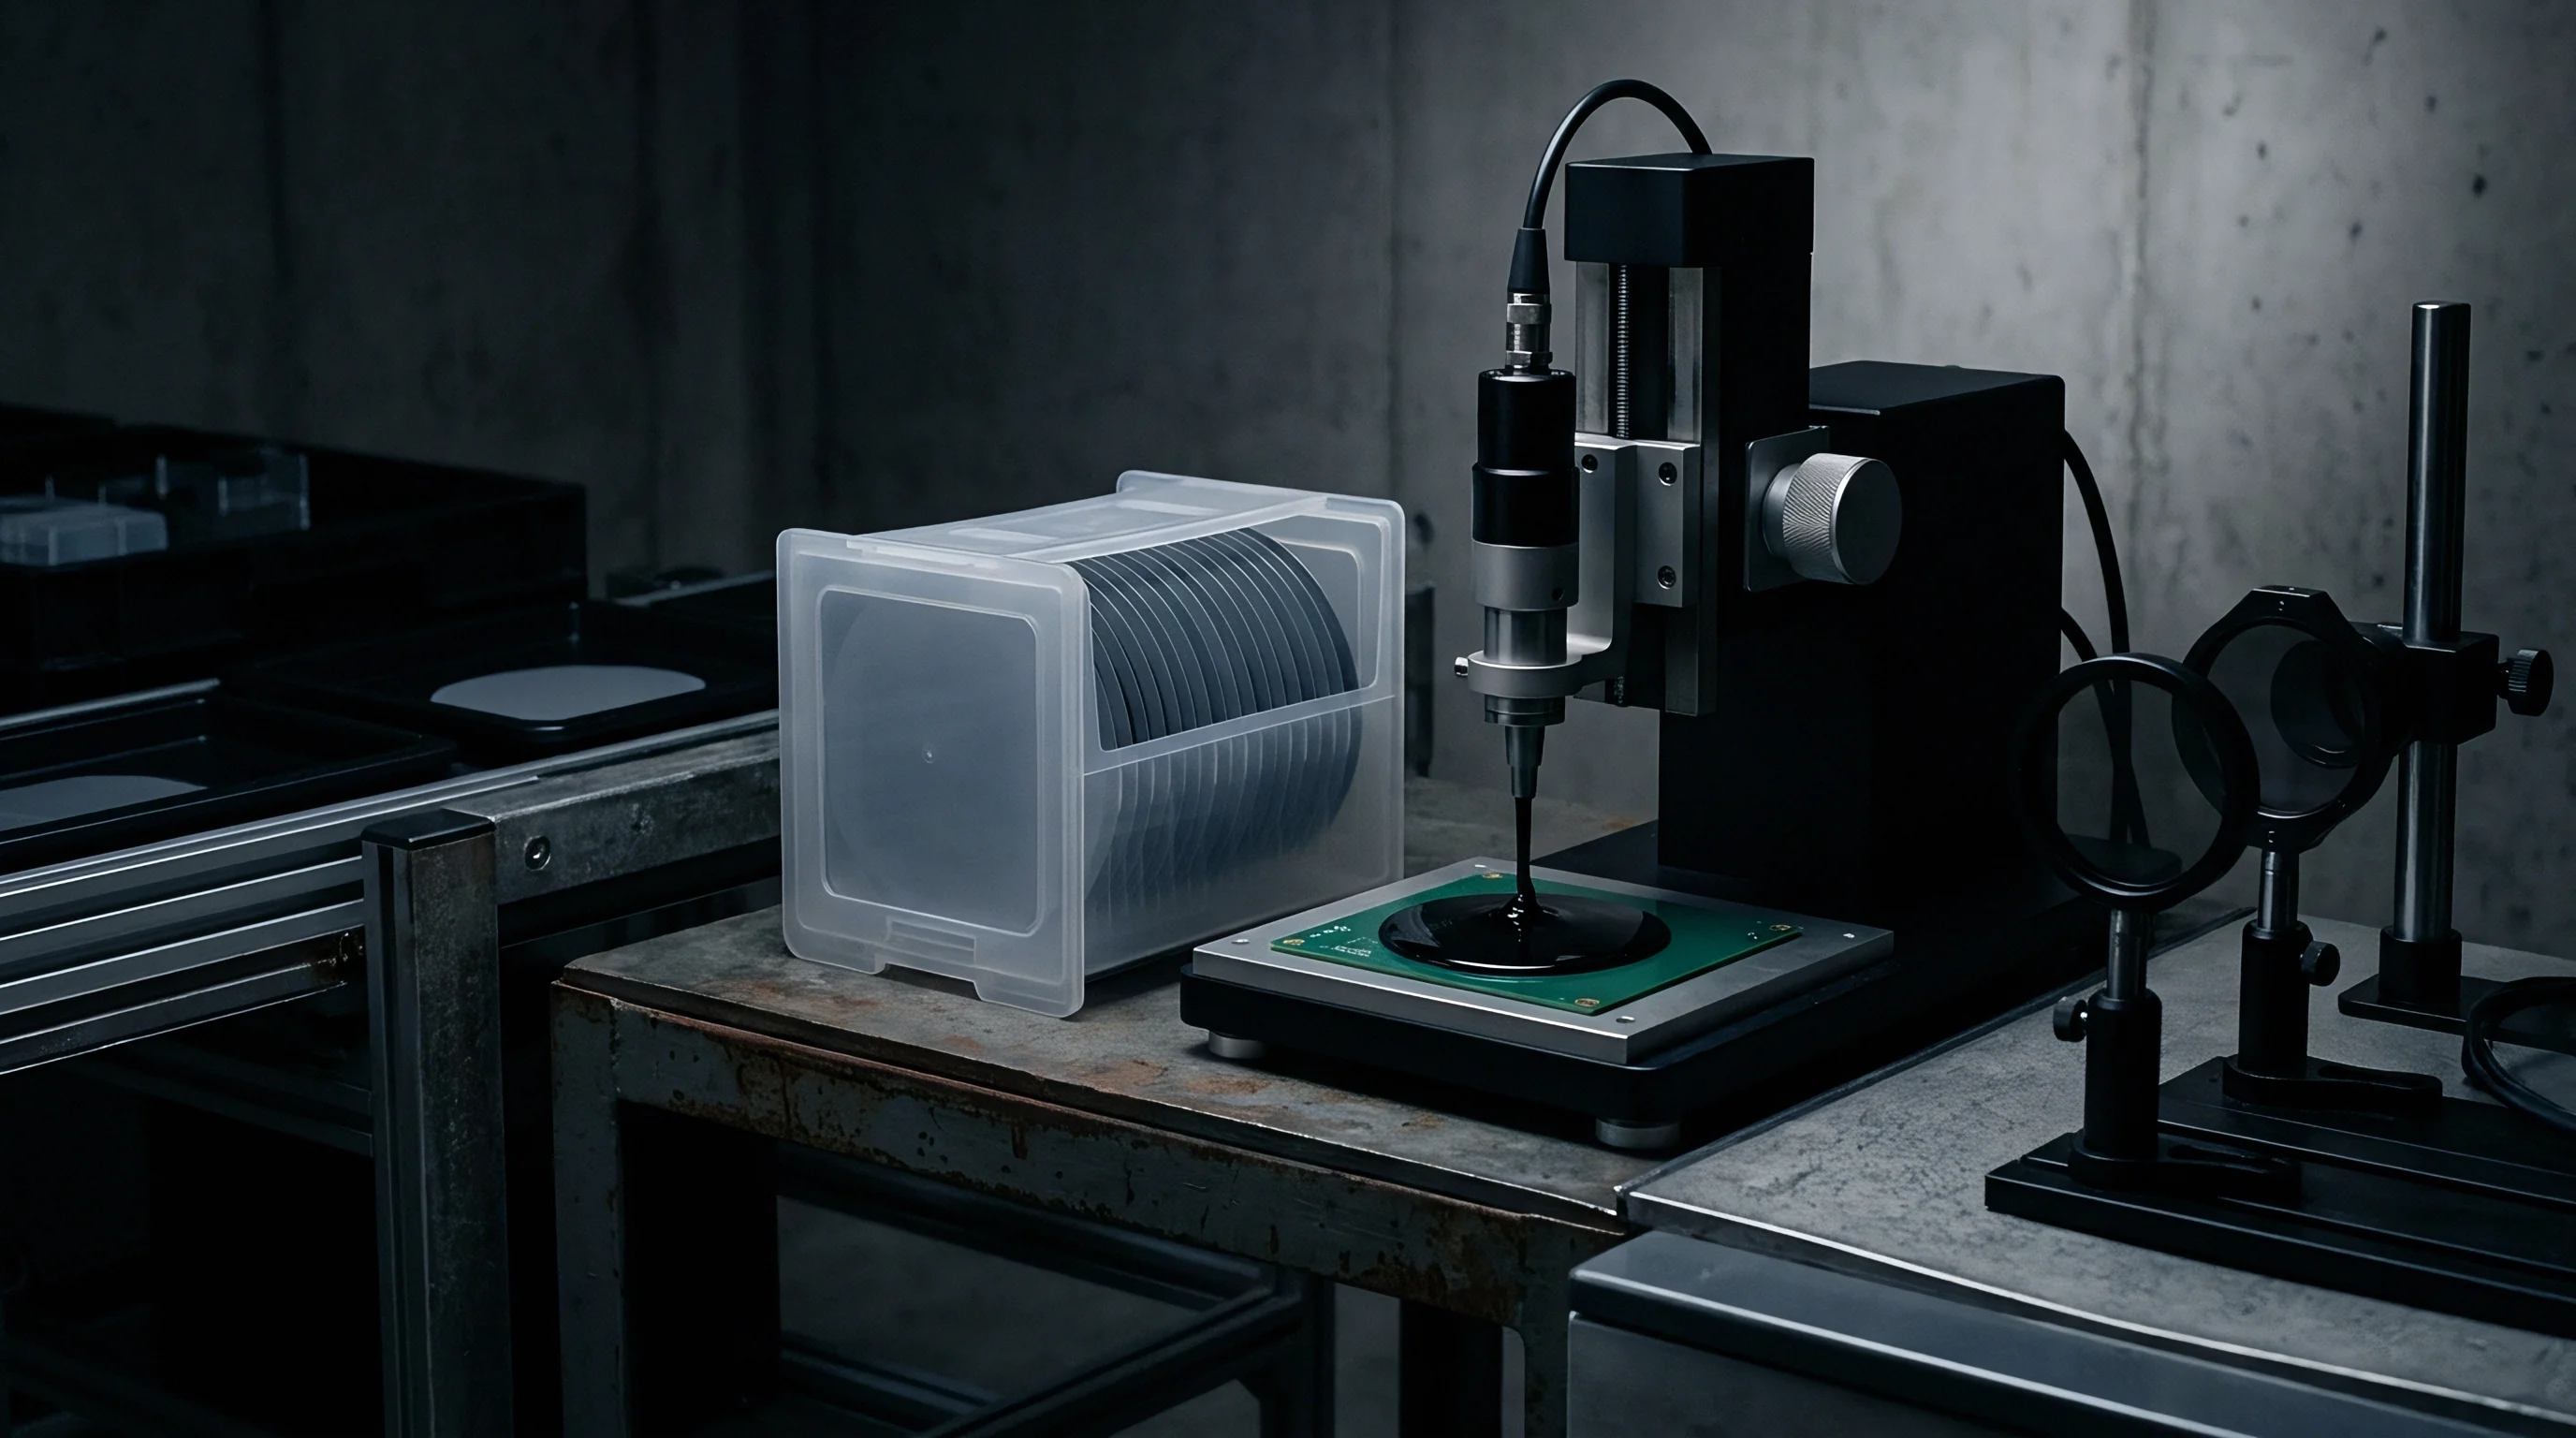
Mitigating mechanical encapsulation stresses requires the insertion of compliant buffer materials between the delicate transducer element and the rigid structural potting. Stress-decoupling buffers act as mechanical low-pass filters, absorbing bulk resin shrinkage and thermal expansion mismatches before shear forces reach active die surfaces or wire bonds. A soft silicone junction coating applied over the sensing element isolates the silicon crystal lattice from external housing distortions, preserving sensor accuracy across wide industrial operating envelopes.
Implementing a dual-layer encapsulation system separates mechanical protection duties from environmental barrier functions. The primary buffer layer directly contacts the die, wire bonds, and passive components, providing an ultra-low modulus interface. The secondary outer potting layer provides chemical resistance, mechanical shock damping, and ingress protection rated up to IP67 or IP69K.
This mechanical decoupling strategy allows instrumentation designers to utilize rugged, highly cross-linked epoxy outer shells without sacrificing the microvolt-level precision of the internal analog sensing core.
Soft Silicone Glob Top Decoupling Layers
Silicone glob tops formulated for stress relief possess Young’s moduli below 2.0 MPa and elongation capabilities exceeding 150 percent. Dispensed directly over the wire-bonded die via automated needle systems, the silicone material flows under gravity to encapsulate delicate interconnects. Capillary action draws the liquid silicone beneath wire loops, creating a void-free compliant envelope.
The glob top is thermally or UV-cured before the secondary structural encapsulation resin enters the housing cavity.
Precise control of glob top dispensing volume is mandatory to prevent buffer migration onto housing seal areas. Excess silicone bleed along circuit board traces inhibits secondary epoxy adhesion, creating liquid leak paths along the connector interface. Modern production lines utilize low-viscosity thixotropic silicone formulations with high yield points, preventing the buffer dome from slumping beyond designated keep-out zones during the pre-cure thermal profile.
Compliant Underfill Layer Thickness and Fillet Height Control
Flip-chip sensor dies and wafer-level chip-scale packages require compliant underfill layers to distribute thermal shear stresses across solder bump arrays. Standard rigid underfills match the CTE of silicon to prevent solder fatigue, but transmit substantial board-level flexure stress directly to the active die face. Highly compliant silicone-modified underfills decouple the die from circuit board warpage induced by high-torque enclosure mounting bolts.
Fillet geometry controls the stress concentration factor at flip-chip corners. A controlled fillet height reaching 75 percent of the die thickness prevents edge chipping under hydrostatic potting pressures. Incomplete underfill dispense leaves voids beneath the die active area, creating localized stress concentrations that induce non-linear pressure transducer output curves under ambient pressure variations.
| Buffer Architecture | Buffer Thickness (um) | Primary Modulus (MPa) | Offset Shift (mV/V) | Thermal Hysteresis (%FS) |
|---|---|---|---|---|
| Unbuffered Rigid Epoxy Baseline | 0 | 6500 | 3.45 | 1.85 |
| Direct Dielectric Gel Coat | 250 | 0.08 | 0.12 | 0.04 |
| Thixotropic Silicone Glob Top | 600 | 1.20 | 0.35 | 0.08 |
| Compliant Silicone Underfill | 45 | 12.0 | 0.65 | 0.15 |
| Dual-Layer Polyurethane Matrix | 400 | 85.0 | 1.20 | 0.42 |
When Does Dual Compound Encapsulation Justify Additional Dispense Steps?
Dual-compound encapsulation introduces substantial capital expenditure and cycle time penalties onto automated production lines. Each dispense operation demands a precision meter-mix dispensing head, optical vision alignment, and dedicated thermal or ultraviolet curing ovens. Adding a secondary buffer step increases line footprint by 3.5 meters and extends work-in-progress cycle times by twelve to twenty-four minutes per pallet.
High-reliability applications justify this capital investment when baseline sensor offset drift without buffering exceeds the total allowable error band defined in the customer procurement specification.
Automotive powertrain sensors and offshore oil instrumentation operate under severe thermal shock regimes where single-compound potting fails consistently. Subjecting an unbuffered pressure transmitter to MIL-STD-883 Method 1010 thermal cycling between -50 degrees Celsius and 150 degrees Celsius induces rapid wire bond shear failures. The inclusion of a compliant primary silicone glob top lowers peak wire bond stresses below 15 MPa, extending fatigue life beyond 2000 thermal shock cycles without signal degradation.
IPC-A-610 Class 3 acceptance criteria mandate complete, crack-free encapsulation coverage around all leaded terminations with zero exposed base metal after cure.
Drift
Long-term sensor drift in encapsulated industrial assemblies stems from the ongoing physical relaxation of polymer chains under sustained mechanical stress. Following the initial chemical cross-linking reaction, polymer networks undergo physical aging, a slow thermodynamic process where polymer segments rearrange toward lower free volume states. Physical aging increases resin density and modulus over months of service, generating continuous, low-level changes in the residual stress field applied to the internal transducer core.
Viscoelastic creep converts elastic stress into unrecoverable plastic deformation over extended operating periods. A sensor calibrated immediately post-assembly exhibits stable zero-point readings for several days, followed by continuous baseline migration as the internal stress field relaxes. Industrial field transmitters deployed in continuous process monitoring must maintain calibration over five to ten years, making polymer viscoelastic creep a primary source of uncorrectable long-term drift errors.
Viscoelastic modulus relaxation in unfilled epoxies causes zero-point output drift of 0.18 percent full-scale span per decade of time in hours at 85 degrees Celsius.
Long Term Modulus Relaxation and Zero Point Migration
The time-dependent modulus of encapsulation polymers follows the Kohlrausch-Williams-Watts stretched exponential relaxation model. At constant operating temperatures, residual stresses relax rapidly during the initial 100 hours of operation before entering a logarithmic decay phase. Piezoresistive pressure sensors and strain gauge bridges convert this changing residual stress directly into an electrical voltage shift, manifesting as steady zero-point drift.
Accelerated aging trials conducted at elevated temperatures allow qualification teams to predict multi-year baseline stability. Holding assemblies at 85 degrees Celsius for 1000 hours accelerates physical aging by a factor of 16 relative to 25 degrees Celsius room temperature operation. Sensing assemblies showing baseline shifts greater than 0.25 percent of full-scale span during this accelerated window require redesign of the buffer geometry or transition to higher filler content encapsulants.
Moisture Swelling Dynamics in Harsh Washdown Environments
Polymer encapsulants absorb moisture from ambient operating environments via Fickian diffusion. Ingressing water molecules occupy free volume between polymer chains and form hydrogen bonds with polar groups in the cross-linked matrix. Moisture absorption induces hygroscopic swelling, expanding the polymer matrix and generating intense compressive stresses against the sensor die.
Water uptake in epoxies ranges from 0.5 percent to 3.0 percent by weight at 85 degrees Celsius and 85 percent relative humidity. Hygroscopic expansion coefficients typically range from 0.15 percent to 0.40 percent strain per weight percent of absorbed moisture. Cyclic washdown cycles in food processing facilities expose sensors to alternating steam cleaning and cold water rinses, driving rapid cyclic hygroscopic stress pulses that mimic high-magnitude mechanical pressure inputs.
Firmware Thermal Compensation Register Updating
Modern industrial sensors combine microcontrollers with internal non-volatile EEPROM registers to store multi-order polynomial compensation coefficients. Factory calibration routines map sensor output across temperature and applied pressure, writing gain and offset correction matrices into register addresses 0x30 through 0x48 over standard I2C or SPI digital interfaces. These fixed polynomial coefficients assume static mechanical housing stresses, correcting only for the intrinsic temperature coefficient of the silicon piezoresistors.
Polymer creep and hygroscopic swelling invalidate static factory calibration coefficients over operating lifetimes. Firmware architectures mitigating this effect incorporate adaptive baseline tracking algorithms. The host controller samples the zero-load state during known process idle states, calculating an offset correction term that updates volatile operational registers without rewriting non-volatile EEPROM cells, avoiding flash memory write endurance limits.
- Pre-condition the unencapsulated transducer through three complete thermal cycles between -40 degrees Celsius and 125 degrees Celsius to relieve raw substrate machining stresses.
- Dispense compliant silicone buffer over the sensing die face, holding a keep-out zone tolerance of plus or minus 0.15 mm from the package header weld perimeter.
- Cure the primary silicone buffer at 100 degrees Celsius for 45 minutes in a nitrogen-purged convection oven.
- Fill the housing cavity with 65 percent silica-filled epoxy, executing dispense in two distinct stages to allow entrapped air bubbles to escape before secondary fill.
- Perform secondary cure at 70 degrees Celsius for 120 minutes followed by an unconstrained post-cure bake at 110 degrees Celsius for 180 minutes.
- Place the fully cured assembly in an environmental chamber at 85 degrees Celsius for 72 hours to complete initial viscoelastic modulus relaxation before executing final multi-point digital calibration.
Does the rate of hygroscopic swelling relaxation match the initial absorption kinetics when ambient relative humidity drops from 95 percent down to 10 percent?
Pricing
Encapsulation architecture directly dictates the bill of materials, manufacturing cycle times, line scrap rates, and final delivered prices for industrial sensing modules. Moving from a standard bare surface-mount component to a fully potted, media-isolated probe assembly multiplies unit manufacturing costs by factors ranging from three to twelve. Sourcing teams evaluate whether the reliability gains of complex multi-stage encapsulation offset the substantial upfront tooling, extended cycle times, and automated dispense machinery capital investments.
Direct component pricing represents only a portion of the total landed cost equation. Bare surface-mount pressure dies supplied in tape-and-reel format cost between 1.80 and 3.50 dollars at 50,000-unit annual volumes. Integrating that same die into an overmolded sensor header with dual-compound silicone buffering, structural epoxy backfill, and an integrated M12 industrial connector escalates unit pricing to 14.50 to 22.00 dollars.
Sourcing managers must balance the internal assembly cost of unpotted modules against the higher purchase price of pre-encapsulated, factory-calibrated standalone probe units.
Single-compound automated potting lines require a minimum volume threshold of 35000 units annually to achieve capital equipment amortization parity against outsourced sub-tier contract encapsulation.
Dispense Automation Cycle Time and Tooling Capital
Automated meter-mix dispensing systems capable of handling highly abrasive, silica-filled two-part resins cost between 85,000 and 160,000 dollars per cell. Piston-pump dispense heads require routine maintenance and seal replacements every 250,000 dispense cycles to prevent abrasive wear from eroding volumetric dosing precision. Dual-compound production lines demand two distinct dispense cells connected by automated conveyor loops and in-line thermal cure tunnels, pushing total work cell capital expenditure beyond 350,000 dollars.
Cycle times govern factory floor capacity. Dispensing structural epoxy into a four-cavity industrial sensor housing requires 18 seconds of active needle motion, followed by 45 seconds of vacuum degassing to eliminate micro-voids around tight terminal pins. Batch curing in large convection ovens consumes two to four hours of line flow, tying up work-in-progress capital.
Ultraviolet-cure acrylic and epoxy formulations compress cure times down to 30 seconds per fixture, but impose a 40 percent raw material price premium and carry high cure-shrinkage stress penalties.
Yield Penalties across Single Cavity versus Panel Molding
Manufacturing sensor assemblies on continuous multi-up PCB panels optimizes surface-mount pick-and-place efficiency, but complicates potting and singulation operations. Dispensing encapsulation resin at the panel level risks cross-cavity resin bleed if solder mask dams or mechanical tooling seals fail. A single dispensing failure or entrapped bubble on one sensor cavity renders the entire panel segment un-singulatable, generating yield penalties that scale geometrically with panel density.
Single-cavity housing encapsulation isolates yield fallout to individual failing units. The labor required to insert individual circuit boards into standalone housings, attach wiring headers, and clamp sealing fixtures increases direct touch labor costs by 1.25 to 2.80 dollars per finished part. High-reliability aerospace and medical sensor manufacturing lines standardise on single-cavity processing to maintain strict traceability and isolate batch contamination risks, accepting lower line throughput in exchange for guaranteed quality metrics.
| Variant Form Factor | Direct BOM ($) | Direct Labor ($) | Tooling Amort ($) | Yield Fallout ($) | Delivered Price ($) |
|---|---|---|---|---|---|
| SMD LGA Sensor Package (Unpotted) | 2.85 | 0.35 | 0.15 | 0.08 | 3.43 |
| Single-Compound Potted Module | 5.40 | 1.85 | 0.65 | 0.32 | 8.22 |
| Dual-Layer Buffer Potted Module | 7.20 | 3.10 | 1.25 | 0.55 | 12.10 |
| Overmolded Cabled Sensor Probe | 11.50 | 4.20 | 2.10 | 0.85 | 18.65 |
| Hermetic Welded Stainless Canister | 18.90 | 6.50 | 3.40 | 1.10 | 29.90 |
Commercial Tradeoffs between Standard Modules and Custom Overmolded Probes
Standard surface-mount sensing packages offer rapid firmware integration and low initial component pricing, but transfer the entire encapsulation engineering burden onto the system integrator. Designing an in-house potting process exposes the buyer to formulation qualification risks, dispense machine downtime, and post-reflow yield loss. Custom overmolded probe assemblies purchased directly from specialized tier-one sensor manufacturers bundle the sensing die, stress buffer, structural encapsulation, and EMC shielding into a single pre-tested part number.
Custom probe variants demand Non-Recurring Engineering investments ranging from 45,000 to 120,000 dollars for injection mold tooling and automated calibration fixtures. Minimum Order Quantities for custom overmolded assemblies typically start at 5,000 to 10,000 pieces per manufacturing lot, creating inventory carrying costs that weigh heavily on lower-volume industrial programs. Sourcing decisions evaluate the break-even volume curve, where high-volume projects amortize custom tooling costs within eighteen months of serial production.
- Material Safety Compliance mandates third-party laboratory verification certificates confirming RoHS 3 and REACH SVHC compliance for all imported resin formulations.
- Potting Process Traceability requires suppliers to log resin batch numbers, mix ratios, vacuum levels, and cure oven thermal profiles against individual serialized part barcodes.
- Yield Loss Compensation defines financial chargebacks where the encapsulating subcontractor credits the full landed value of buyer-furnished populated circuit boards destroyed by potting voids.
- Shelf Life Guarantees ensure two-part polyurethane and epoxy raw materials maintain specified viscosity and gel time parameters for a minimum of six months from receipt.
A compliant silicone buffer layer consistently prevents structural epoxy cure shrinkage from destroying sensor bridge calibration.