Automated JTAG Boundary Scan Architecture for Heterogeneous Package Assemblies
Automated boundary scan architecture isolates microbump faults inside multi-die packages, replacing physical probing to safeguard assembly yields.
Bridge
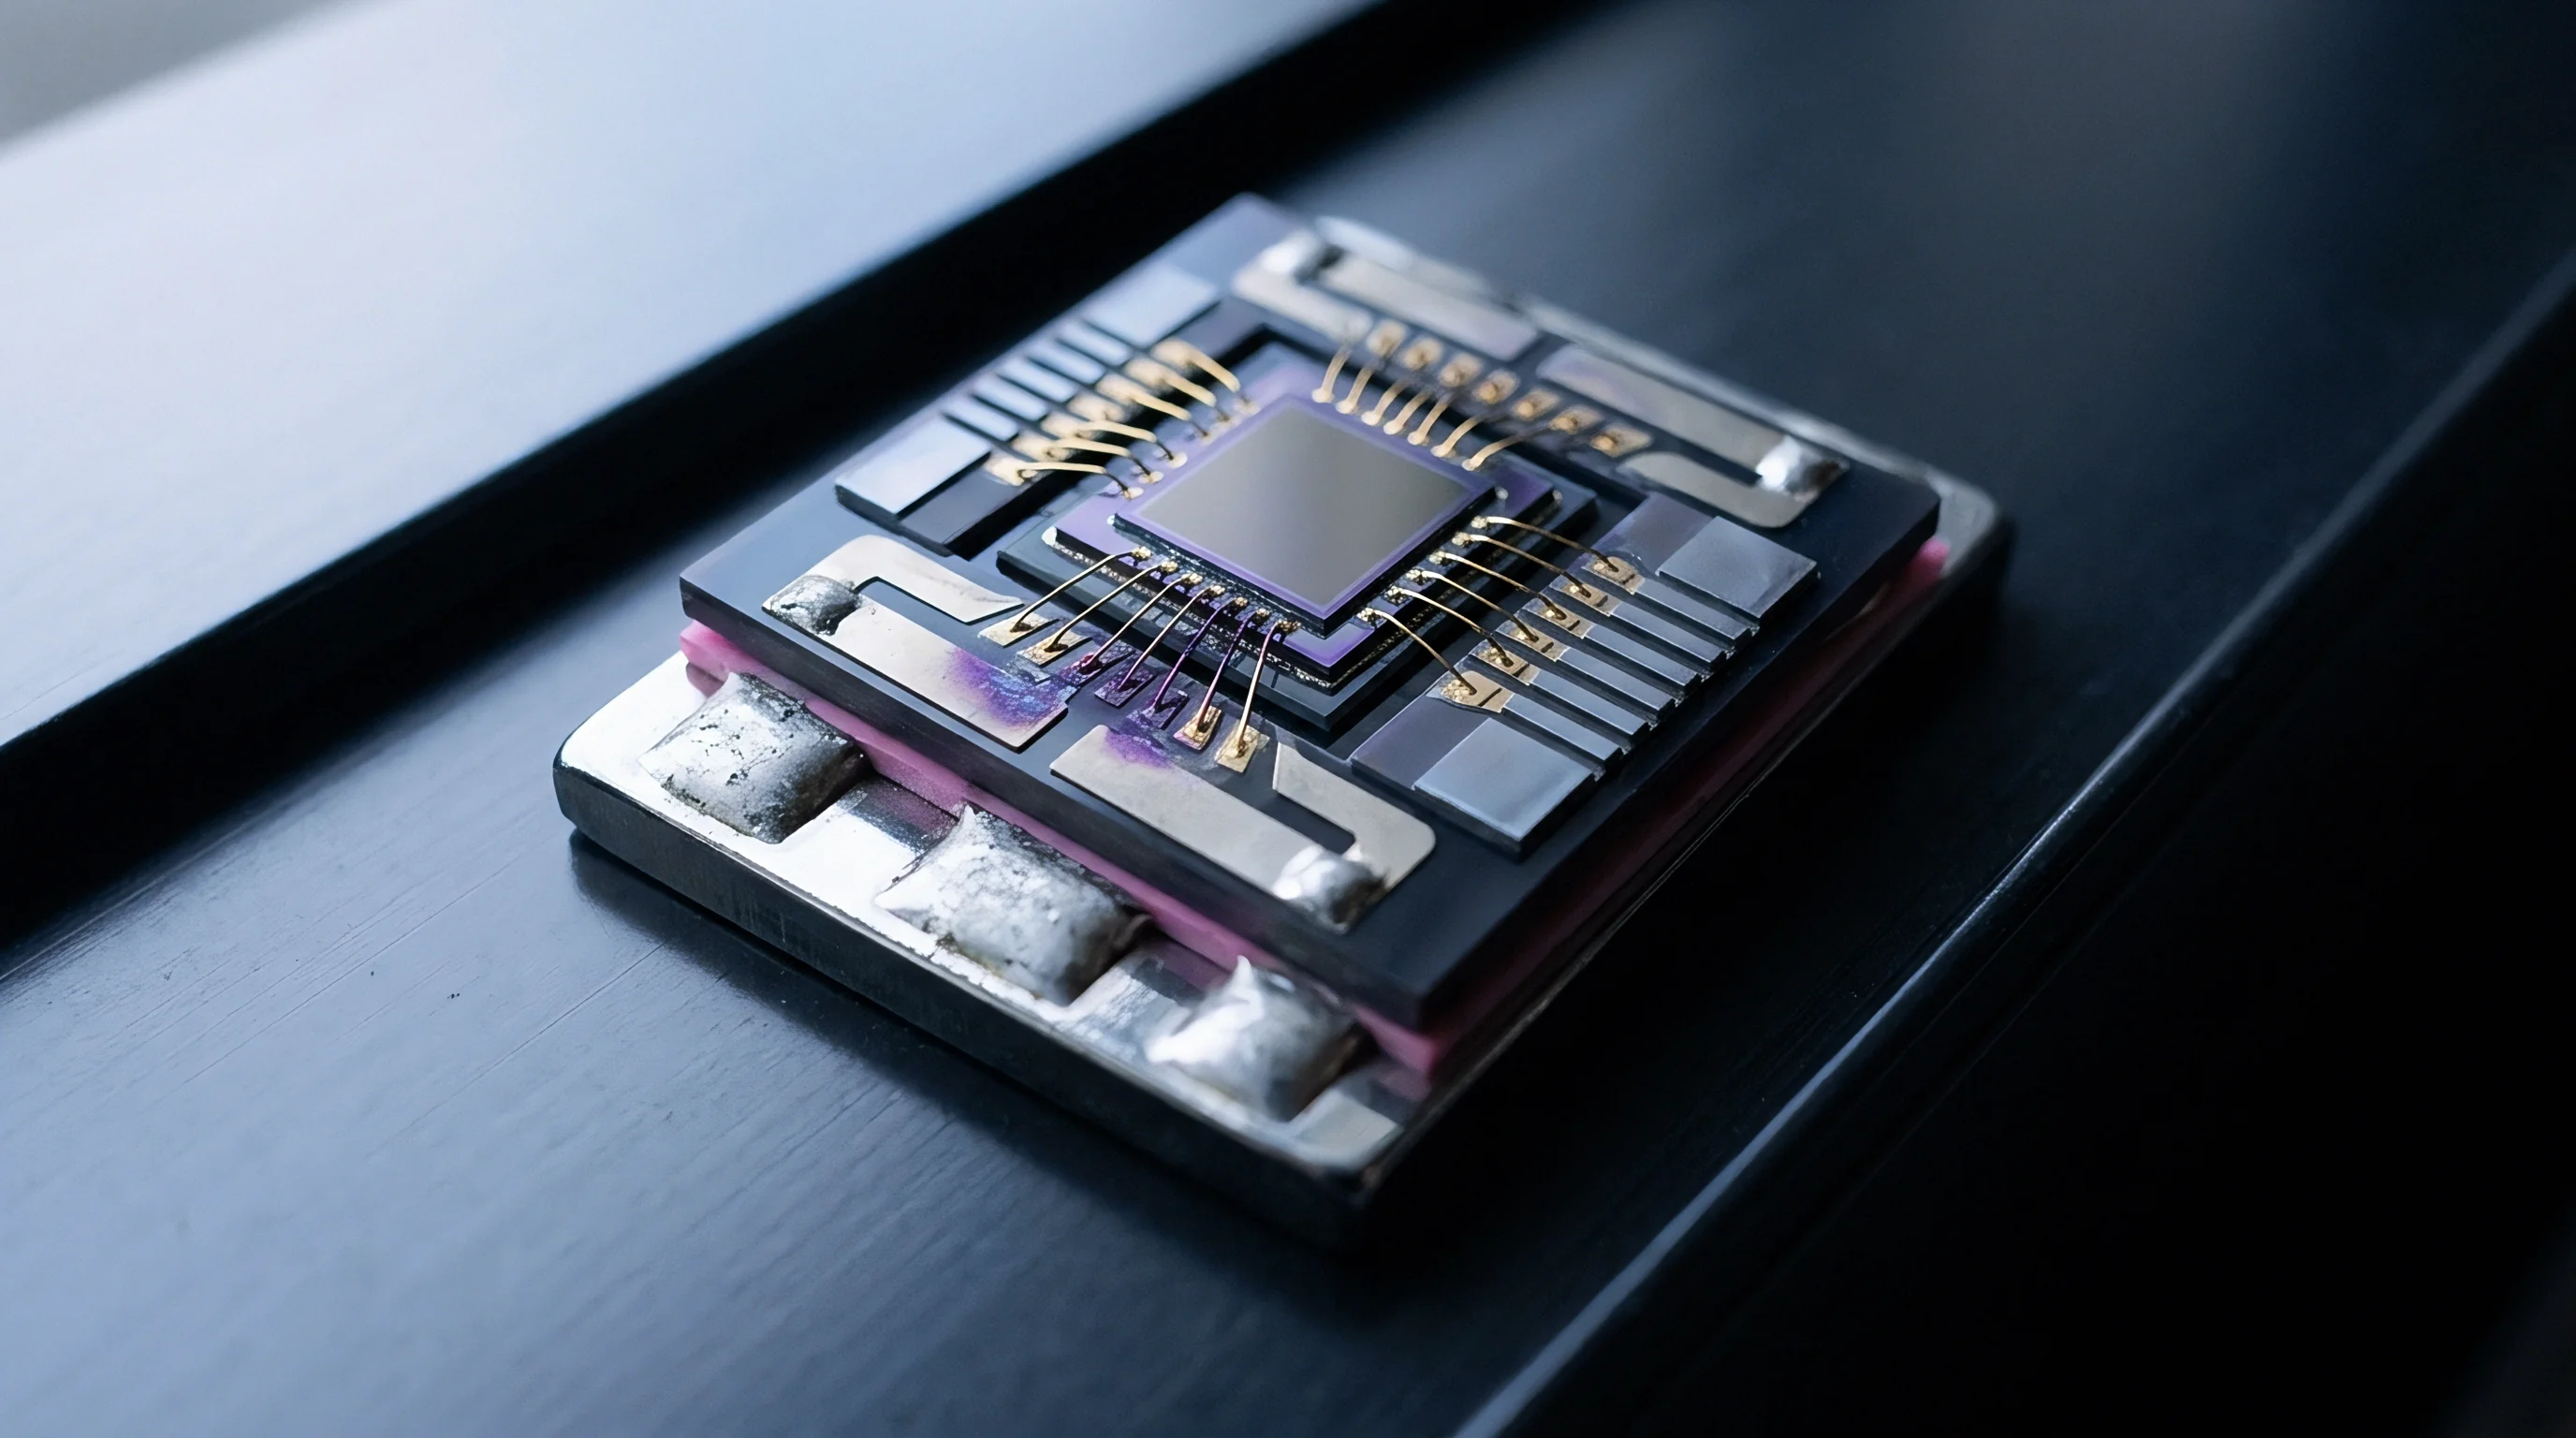
Modern multichip modules pack separate functional dies onto high-density interposers using microbump grids pitched between 25 and 55 micrometers. Physical needle probes fail at these dimensions. Mechanical contact cards damage fine-pitch solder pillars, skate across bond pads during thermal expansion, and induce dielectric cracking beneath fragile copper traces.
Solder joint failures stay invisible once underfill flows between the dies. Multi-die packaging shifts assembly verification from mechanical bed-of-nails probing to internal digital scan paths.
Heterogeneous integration brings together bare processor dies, radio frequency transceivers, high-bandwidth memory stacks, and MEMS sensors on a single substrate. Each component arrives from different wafer fabrication nodes with distinct thermal expansion profiles, varying operating voltages, and proprietary test logic. Substrate warpage during reflow shifts bump coplanarity by up to 12 micrometers across a 30-millimeter package span.
Thermal warpage snaps fine microbumps. Open circuits appear along outer interconnect rows where shear stresses peak. Without dedicated test circuitry embedded directly into the die pads, assemblies with twenty good chiplets fail from a single fractured interposer trace.
A 40-millimeter interposer running a 35-micrometer microbump pitch tolerates no more than 6 micrometers of dynamic out-of-plane warpage during reflow before peripheral bump solder opens appear.
Embedded boundary scan architecture replaces direct pin probing with scannable shift registers placed at every chiplet input and output pad. Standardized boundary cells capture state, force drive voltages, and route serialized vectors through package traces. The automated boundary scan path links multiple silicon dies across embedded bridges and redistribution layers.
Scan vectors isolate open solder joints, solder bridges, and damaged input-output buffers before final system encapsulation.
Physical Access Limits in Dense Packages
Wafer redistribution layers route hundreds of interconnect lines per millimeter of die edge. Line spaces fall below 1.5 micrometers on modern organic interposers and reach sub-micron geometries on passive silicon carrier substrates. Solder bumps occupy lands measuring 20 to 30 micrometers across.
Flying probes and cantilever probe cards cannot touch these internal nets without destroying the package metallurgy. Mechanical test points add parasitic capacitance that degrades high-frequency differential signals running above 16 gigatransfers per second.
Direct interconnect probing collapses under fine pitch constraints. Microbump pitch dictates probe clearance. Scan cells placed inside the physical layer macro handle verification over software interfaces.
The boundary register captures interconnect values at the transmitter pad and transfers them along the boundary chain, bypassing exterior mechanical fixtures. Digital scan tests execute at lower clock rates between 10 and 50 megahertz, confirming structural connectivity before the product powers up high-speed parallel links.
Structural Interconnect Fault Topologies
Packaging stresses generate specific failure modes along chiplet boundaries. Thermal expansion mismatches between the silicon die, underfill material, and organic substrate generate high mechanical strain at package corners. Solder pillars separate during cooling, creating open joints.
Excess solder paste or misalignment causes bridging across adjacent microbumps. Dielectric breakdown inside redistribution traces creates high-resistance leakage paths to ground planes.
Microbump interconnect defects fall into distinct physical classes across heterogeneous substrates:
- Microbump open circuits break physical continuity when solder fails to wet or separates under tensile warpage.
- Solder bridging faults short adjacent signal paths together through displaced solder volume or foreign metal debris.
- High-resistance joints throttle current delivery through fractured intermetallic compound layers, causing intermittent voltage drops.
- Redistribution layer shorts tie high-speed signal tracks directly to adjacent power rails through substrate fabrication pinholes.
Boundary scan patterns exercise these traces by applying walking patterns, checkerboard sequences, and polarity inversions across die-to-die lanes. The test logic drives complementary states on neighbouring traces to expose capacitive crosstalk and resistive bridging. Measuring output response codes against expected netlists confirms physical interconnect health across the multi-die substrate.
Router
Coordinating boundary scan registers across stacked and tiled silicon dies demands a structured hierarchy of test access ports. The classic IEEE 1149.1 standard provides a four-wire or five-wire serial bus intended for single-chip board designs. Heterogeneous multi-die assemblies demand internal switching networks that traverse vertical through-silicon vias, silicon bridges, and high-density substrates without inflating package pin counts.
Modern multi-die test architectures combine IEEE 1149.1 package-level interfaces with IEEE 1500 core wrappers, IEEE 1687 internal JTAG networks, and the IEEE P1838 standard for 3D stacked ICs. The primary Test Access Port (TAP) controller accepts external serial vectors at the package balls and directs them to secondary controllers located within individual chiplets. Test data registers select specific dies for boundary testing, bypass unaffected components, and read out environmental sensor telemetry.
Test access multiplexers route vectors across complex die arrangements. Routing density forces trade-offs. Designers place distributed TAP routers on passive interposers or inside base dies to govern local scan loops.
Dynamic scan segment selection isolates broken dies, allowing test programs to complete interconnect verification across remainder channels.
Hierarchical Access Standards
The IEEE 1500 standard establishes dedicated wrapper boundary registers around embedded cores and individual chiplets. A standard IEEE 1500 wrapper includes an instruction register, a wrapper bypass register, and wrapper boundary cells operating in wrapper-instruction and wrapper-data modes. Each wrapped chiplet exposes Wrapper Parallel Port or Wrapper Serial Port lines for vector feeding.
Wrapper serial instructions isolate the chiplet core from its periphery, allowing external interposer interconnect tests without toggling internal core logic gates.
The IEEE 1687 standard extends this architecture by treating on-chip instruments as dynamic data registers within the boundary scan chain. Segment Insertion Bits (SIBs) open and close secondary scan loops on demand. A master scan controller configures the active path by loading serial instructions that activate specific SIB gates.
Scan length varies dynamically based on test requirements, shortening test times during high-volume production screening.
Three-dimensional integrated circuits stack multiple active layers using through-silicon via arrays. The IEEE P1838 standard formalizes access mechanisms for these vertical topologies through three defined components:
- Flexible Test Access Port converts primary TAP signals into scalable serial protocols suited for stacked vertical architectures.
- Die Test Interconnect routes scan paths and control lines across vertical through-silicon via pillars between stacked dies.
- Embedded TAP controllers decode local instructions and manage boundary wrappers for each separate vertical die stratum.
Standard IEEE P1838 compliance requires vertical test chains to sustain serial scan operations even when upper-layer dies in the stack lack final power supply connections.
Secondary Controller Architectures
Primary package balls connect directly to the package-level TAP interface. Secondary TAP controllers sit inside memory dies, processor chiplets, and mixed-signal peripheral devices. When the package controller drives an interconnect test, secondary controllers switch into external test mode, driving their respective wrapper boundary cells against the shared redistribution traces.
System designers configure secondary controllers in serial, star, or hierarchical bus topologies. In serial chains, Test Data In (TDI) passes through every chiplet sequentially before returning through Test Data Out (TDO). A broken trace in any single chiplet disconnects the entire scan ring.
In star and hierarchical networks, an addressable router on the central base die directs scan data to specific chiplets using dedicated enable lines. Defective components decouple without terminating package-level diagnosis.
| Standard Designation | Target Assembly Architecture | Interface Width | Maximum Scan Rate | Fault Isolation Mechanism |
|---|---|---|---|---|
| IEEE 1149.1 | Monolithic Package and PCB | 4 or 5 Pins | 25 MHz | Boundary Register Shift |
| IEEE 1149.6 | AC-Coupled High-Speed Links | 4 or 5 Pins | 50 MHz | Pulse-Based Boundary Cell |
| IEEE 1500 | Embedded Core and Chiplet | Serial or Parallel | 100 MHz | Wrapper Boundary Isolation |
| IEEE 1687 | Internal Embedded Instruments | Hierarchical Serial | 50 MHz | Segment Insertion Bit Loops |
| IEEE P1838 | 3D Stacked Die Assemblies | Scalable Serial / DTI | 75 MHz | Flexible TAP Layer Routing |
Selecting the secondary controller topology dictates test vector execution speed and software overhead. Star configurations protect test integrity during multi-die bring-up stages. Boundary scan chains that split into reconfigurable parallel lanes maintain overall diagnostic flow across partial package builds.
Silicon
High-speed chiplet assemblies link compute elements using standardized die-to-die physical interfaces. Protocols like Universal Chiplet Interconnect Express (UCIe), Bunch of Wires (BoW), and Advanced Interface Bus (AIB) route thousands of raw digital lines over short distances at high densities. Silicon interposers break down without inspection.
Ensuring trace health across these ultra-dense channels demands boundary scan circuits engineered directly into high-speed physical layers.
Die-to-die PHYs operate with trace lengths under 25 millimeters and line pitches below 40 micrometers. These physical dimensions eliminate conventional discrete boundary scan cells due to stringent area and capacitance budgets. A standard boundary cell contains multiple flip-flops and multiplexers, consuming silicon floorplan area and introducing significant trace delays.
Modern D2D interfaces build test cells directly into the analog transmitters and receivers.
Boundary scan cells embedded in UCIe physical layers support DC parametric testing, continuity verification, and real-time lane remap routines. When manufacturing reflow bridges two high-speed data lines, the boundary scan engine flags the physical coordinate of the shorted microbump. Diagnostic systems evaluate trace conditions before clock distribution loops commence operation.
Will Interposer Routing Density Constrain Scan Paths?
Passive silicon interposers feature routing spaces down to 0.8 micrometers, approaching standard semiconductor gate dimensions. High wire counts choke available escape channels around package centres. Adding dedicated serial scan traces alongside thousands of high-speed data tracks introduces severe routing congestion.
Test vectors grow exponentially.
Engineers solve escape congestion by combining shared boundary cells with serialized scan backbones. Instead of routing independent scan controls to every bump pad, physical layer macros integrate shift logic inside the transmission line drivers. Test data shifts through parallel data lanes during manufacturing test mode, repurposing functional data nets as scan paths while off-line.
Microbump arrays eliminate redundant routing by multiplexing functional clock trees into boundary scan scan-clock distribution trees.
Boundary Cell Design in High-Speed PHYs
Conventional IEEE 1149.1 boundary scan cells insert multiplexer logic directly in the primary signal path between the core logic and the output driver pad. This series switch introduces propagation delay, adding jitter and limiting operational frequencies on links running above 10 gigabits per second. High-speed transceivers abandon series multiplexers in favor of parallel, non-intrusive test sampling circuits.
A non-intrusive boundary scan cell taps the transmitter pre-driver and receiver comparator without placing logic elements directly in line with functional signals. In normal operating mode, test circuits remain powered down or high-impedance. During test execution, dedicated drive circuits force static test levels onto the pad, while auxiliary capture latches evaluate received logic voltages.
Test operations execute without degrading functional signal integrity during high-speed missions.
A transmission channel running 16 gigatransfers per second tolerates no more than 15 femtofarads of added parasitic capacitance from test tapping logic before channel eye margins degrade beyond acceptable link budget limits.
AC-coupled links require specialized boundary scan cells complying with IEEE 1149.6. Pure DC scan vectors cannot cross series blocking capacitors placed between driver pins and interposer tracks. IEEE 1149.6 receiver cells integrate transition-detection filters and edge-capturing latches.
These circuits fire on logic transitions, measuring low-frequency and high-frequency edge performance across the coupling capacitors to verify solder joint integrity on AC-isolated lanes.
Interconnect test standards define performance minimums for boundary scan implementations across modular assemblies. IEEE Standard 1149.6 Section 5 specifies edge-detector signal margins and pulse durations, mandating precise signal transition testing for high-speed differential pins to verify solder continuity through external capacitor components.
Vector
Test pattern generation converts package netlists into bit streams executed on high-throughput automated test equipment. Heterogeneous packages complicate vector development because each chiplet brings its own Boundary Scan Description Language (BSDL) file, and internal package routing lacks fixed physical pinouts. Bridging faults escape standard logic.
Automated test pattern generation (ATPG) tools read the composite netlist of the interposer along with BSDL descriptions from each die supplier. The software maps interposer nets, identifies driver-receiver pairs, and synthesizes test vector sets that cycle every interconnect node. Boundary scan test programs verify that every pin drives a distinct logic state while neighbouring pins stay inverted, identifying shorts, opens, and stuck-at faults across every die-to-die channel.
Production testers load patterns into package memory via the TAP interface at frequencies between 10 and 50 megahertz. Scan controllers shift test stimulus through TDI pins, trigger an update cycle that latches voltages onto package pads, and execute a capture cycle that stores incoming states into receiver boundary cells. The shift engine pulls the captured response out through TDO, comparing output bits against expected simulation values in real time.

BSDL Modeling for Multi-Die Netlists
BSDL files define the internal boundary scan register structure, instruction codes, and pin-to-pad mappings for single-chip packages. In heterogeneous modules, chiplet pins connect directly to internal interposer traces without surfacing at external package balls. Conventional single-chip BSDL files fail to represent these internal blind nets.
Hierarchical BSDL and Procedural Description Language (PDL) frameworks define interconnect topology across multi-die packaging. Hierarchical BSDL wraps each sub-die model within a unified package description file. The file details internal connectivity, secondary TAP register locations, and multiplexer routing paths.
Software automated tools parse the hierarchical model, translating high-level board diagnostic routines into localized scan sequences targeting specific silicon interfaces.
| Fault Condition | Applied Test Vector | Observed Logic Response | Diagnostic Register State |
|---|---|---|---|
| Open Microbump Trace | Alternating 1010 Bit Sequence | Floating Input, Static 1 or 0 | Capture Register Stuck High |
| Adjacent Trace Bridge | Complementary Drive Patterns | Matched Logic on Both Lines | Wired-AND / Wired-OR Match |
| High-Resistance Solder Pillar | High-Speed Transition Pulse | Delayed Signal Latch Arrival | Intermittent Capture Flag |
| Redistribution Layer Short | All-Zero and All-One Sweeps | Fixed Ground or Supply State | Stuck-at-Zero or One |
Diagnosing package failures requires deterministic vector sets. Diagnostic software runs walking-one and walking-zero algorithms across interposer traces. A walking-one pattern places a logic high on a single channel while all surrounding traces remain low.
If an adjacent trace registers a high value during the capture cycle, the diagnostic engine isolates a solder bridge between those specific physical coordinates.
Automated Localization and Diagnostic Extraction
Package rework and yield analysis demand pin-level fault localization. High-density multichip modules cannot undergo destructive deprocessing for routine diagnostic feedback. Assembly floors demand instant diagnostics.
Automated boundary scan software correlates capture register error signatures directly with physical interposer layout files, highlighting defective microbumps on computer-aided design drawings.
Diagnostic tools export failure coordinates in standard wafer mapping formats. Technicians use this data to inspect specific microbumps via high-resolution X-ray laminography or acoustic microscopy. Automated diagnostics eliminate manual fault mapping across thousands of interposer connections, shortening process tuning cycles on new assembly lines.
Silicon suppliers frequently maintain that unverified internal scan chains are non-essential because final system-level functional boot tests will screen out any defective interconnects during post-assembly burn-in.
Overhead
Integrating boundary scan logic introduces physical silicon penalties and electrical design compromises. Dedicated TAP pins consume package substrate area. Internal wrapper cells consume silicon floorplan resources on active dies.
Scan routing inflates routing metal layer counts on passive interposers.
Design teams evaluate trade-offs between test coverage and die overhead before freezing package floorplans. In high-volume consumer modules, adding four or five dedicated test pins to an area-constrained package represents a prohibitive cost penalty. Package designers mitigate physical pin overhead by multiplexing JTAG signals onto functional low-speed control pins, using custom power-on reset sequences to differentiate between test entry and functional operation.
Test time on automated test equipment scales directly with scan chain length. Long boundary chains take substantial time to shift vectors through tens of thousands of internal cells. Package test costs multiply rapidly.
At high production volumes, every additional second of test duration reduces line throughput and inflates unit manufacturing expenses.
Could Redundant Boundary Cells Protect Package Yield?
High-density packaging features yield loss driven by microbump solder defects. Fabricating spare interposer traces and redundant microbumps allows automated lane remap operations. When boundary scan diagnostics detect an open solder pillar during wafer-level or module testing, internal remapping multiplexers disconnect the broken lane and shift traffic to a spare line.
Redundant boundary scan cells incorporate electronic fuse registers or non-volatile configuration memory. During production screening, scan controllers run automated interconnect tests. If the scan program flags a failing line, the tester writes programming pulses to internal fuse circuits, permanently redirecting data paths around the defect.
Redundancy systems recover assemblies that would otherwise hit scrap bins, offsetting the initial silicon area penalty required for spare cells.
Silicon Area and Test Economics
The cost of test logic scales with chiplet complexity and package density. A standard IEEE 1500 wrapper boundary cell consumes approximately 15 to 30 logic gates. On a wide-interface die featuring 2,048 interconnect channels, boundary cells demand over 50,000 equivalent gates.
This logic overhead represents less than 0.1 percent of an advanced compute die, but it consumes up to 5 percent of the total area on compact mixed-signal or sensor interface chiplets.
Worked financial models highlight these economic trade-offs across volume tiers. Consider a heterogeneous package assembly containing four functional chiplets with a base silicon bill of materials totaling 120 dollars:
- Interconnect fault escape rate reaches 1.5 percent without embedded boundary scan, causing module failure during expensive final system board assembly.
- Scrapped finished modules cost 180 dollars per unit when complete packaging, substrate, and assembly expenses factor into the loss.
- Boundary scan test insertion adds 1.20 dollars in silicon area and increases test duration costs by 0.85 dollars per unit on automated test equipment.
- Yield recovery through automated remapping preserves 80 percent of otherwise failing modules, reducing overall scrap rates from 1.5 percent to 0.3 percent.
At an annual volume of 500,000 units, the initial boundary scan investment saves over 800,000 dollars in scrapped modules, proving its economic value despite silicon area growth. Open interconnects destroy entire assemblies. Implementing structured boundary scan testing converts catastrophic module yield loss into manageable fabrication overhead.
Omitting boundary scan verification from high-density multi-die packages causes undetected solder joint micro-cracks to pass into downstream production lots, driving up warranty claims and field return costs when thermal fatigue turns marginal contacts into permanent electrical opens.
Settlement
Procuring dies for heterogeneous package assemblies requires strict commercial alignment between chiplet vendors, packaging houses, and system integrators. Known good die strategies collapse. A single marginal chiplet ruins all functional partners on the shared interposer.
Sourcing specifications mandate comprehensive boundary scan architectures to establish liability boundaries across production partners.
Procurement agreements define explicit test coverage thresholds for supplied bare dies. Sourcing teams enforce boundary scan compliance by requiring suppliers to ship validated BSDL models, fault dictionary tables, and IEEE 1500 wrapper test vectors with every wafer lot. Contract clauses establish clear liability if an unverified internal die defect causes finished multi-die module fallout during package integration.
Wafer-level probe tests execute initial boundary scan sequences before wafer dicing. Packaging foundries repeat these scans after interposer placement, verifying interconnect health before applying permanent epoxy underfill. If an interconnect fails boundary test before underfill dispensing, the packaging line removes and replaces the defective die using localized rework fixtures.
Interposer yield decides gross margins. Once underfill cures, the package structure becomes permanent, and any hidden solder failure causes complete assembly write-offs.
Known Good Die Qualification Criteria
Known Good Die (KGD) sourcing contracts specify boundary scan structural testing at wafer probe. Chiplet suppliers run internal self-tests through wrapper boundary cells, validating drive strength, input threshold margins, and logic switching states. Wafer probing with fine-pitch microbump arrays remains technically challenging, leading suppliers to execute partial test suites before shipping bare dies.
Procurement contracts protect buyers by establishing acceptable quality levels based on boundary scan fault coverage metrics. Buyers require suppliers to demonstrate minimum single stuck-at fault coverage of 98 percent across all input-output pad cells, alongside complete dynamic toggle coverage for high-speed physical layers. Dies arriving without verified boundary wrappers carry higher yield risk, forcing assembly lines to discount the finished module value or demand vendor yield rebates.
| Assembly Stage | Test Execution Method | Defect Detection Focus | Economic Consequence of Failure |
|---|---|---|---|
| Wafer Probe (KGD) | Membrane Probe Card + TAP | Internal Die Core and PHY Faults | Discard Single Die at Wafer Level |
| Post-Placement (Pre-Underfill) | Package Substrate TAP Scan | Microbump Solder Opens and Shorts | Die Rework and Placement Correction |
| Post-Underfill Curing | Full Boundary Interconnect Test | Thermomechanical Solder Fractures | Scrap Entire Multichip Module |
| Final Package Assembly | Multi-Standard System Scan | Package Ball Ball-Grid Array Continuity | Scrap Module and Substrate Carrier |
Executing boundary scan checks at early assembly stages preserves capital. Reworking a single misplaced die before underfill application costs a fraction of the expense incurred when scraping a completed package assembly. Structured test architectures protect commercial margins across complex multi-die production operations.
Contractual Test Coverage Clauses
Master supply agreements for chiplets incorporate specific clauses governing test data delivery, BSDL model validation, and boundary scan coverage levels. Sourcing managers write clear language into purchase orders to hold die suppliers accountable for assembly fallout caused by latent silicon defects. These specifications define the diagnostic tools, vector sets, and interface protocols necessary to confirm component viability across shared assembly lines.
Standard purchase terms require suppliers to provide validated test vectors that achieve complete structural coverage of all die-to-die physical interfaces prior to initial volume shipments. When suppliers fail to deliver working BSDL models or omit boundary scan cells on critical interconnect lanes, buyers lose the automated diagnostic capability needed to localize defects. Resolving these operational blind spots determines how multi-die integration platforms manage financial risk between silicon suppliers and outsourced assembly providers as bump pitches drop below 10 micrometers.